
Molten metal and casting
as of 0.8.0
Molten metal is plumbed, never carried in a bucket or a stack. It leaves a furnace tap into a canal and flows cell by cell to wherever the canal was built to go, and it is cast at the far end. The one thing a player does carry is a filled mold, and that is where the burns come from.
The canal run
A canal is not a pipe with one shared pool. Each block owns the metal standing in it, and each second some of it moves to the next cell along.
| Quantity | Value |
|---|---|
| capacity of one canal block | 50 units |
| flow across one connection | up to 50 units per second |
| smallest transfer worth making | 10 units |
| drain speed at a canal tap or mold pedestal | 20 units per second |
| Shank ladle capacity | 600 units |
| large mold capacity | 100 units |
| cooldown toward ambient | 24 C per second, toward 20 C |
Because every cell is its own vessel, a long canal takes visible time to deliver, and a canal left standing full goes solid where it stands. Flow direction is decided by which of two neighbouring cells holds more, not by which end the furnace is at, so metal runs back toward the canal start whenever the downstream cell is fuller. A level canal pushes a pour on toward its end and leaves a 10 unit skin in every cell once the pour stops, every cell must touch the next, and a gap stops the run; a slope runner carries metal down.
The family is four transport shapes and three endpoints. The canal start sits under a furnace tap and takes the runout, and it is also a valid target for a hand pour from a vanilla smelted crucible. A cast Canal Plate is the run's valve: with the plate in one hand and a hammer in the other, a click on a straight, bend, tee or cross drives it into the joint nearest the click, and the run is cut there. The plate goes in whether or not the cell holds metal, and nothing is lost: the metal behind it backs up and the metal ahead of it runs on. Tongs on the plate draw it out again and the two sides level. A plate cannot be driven into or drawn out of a cell that has frozen solid; chip the plug out first.
Coloured running brick and fire brick each make the whole family of canal shapes, laid at the Vice Bench round the canal diagram, and which of them a run is built from is cosmetic; see Diagrams and the drawing table.
The three exits
Molten Canal (Tap) pours down into whatever is parked beneath it. A plain right-click with a dried Shank Ladle or a large tool mold in hand parks it; sneak plus right-click with an empty hand retrieves what is parked with its contents; ctrl plus right-click toggles pouring. Parking needs a real solid surface directly below. A ladle takes metal even after the metal in it has hardened, because it re-melts; a mold does not, because a hardened mold is a finished cast.
Molten Canal (Mold Pedestal) fills one small tool mold standing on it, on the same modifier scheme. It drains the run straight into the mold at most 20 units per second, as the tap does.
The sand casting stations pull metal out of an adjacent cell themselves rather than being poured into. The Small Flask and the Sand Casting Bed pull 50 units per tick from the face they are drawn to take it on.
Heat, molds and burns
Clay is the ceiling of the ceramic tier. A small fired-clay tool mold shatters instead of casting when the metal poured into it is above 1340 C, the hottest a vanilla firepit heats a crucible, so it bites only on metal from an iiex furnace. It shatters with no drop and a crack that every player within 8 m hears. Large anvil and helve-hammer molds are exempt, and the mod's own Cast Iron Ingot Mold never shatters.
A filled mold can be picked up, which vanilla's cannot. Two things follow:
- Carrying one bare-handed burns at 200 C of content and above. Gloves stop it; tongs do not, and never will, because a mold is held in two hands.
- A mold taken into anything but an empty hand spills. Put it in the active slot and leave it there until it is set.
The mod's own cast molds always have this handling. Vanilla clay tool molds get it only when
EnhanceVanillaMolds is turned on, which is off by default; turn it on live with
/exmod config iiex EnhanceVanillaMolds true.
A cast-iron mold body soaks up 0.7 of the poured metal's temperature as its own glow and sheds it at 25 C per second. Pulling a mold off a pedestal and setting it on the ground cools the cast faster than leaving it under the run.
Sand casting
Sand casting is the route out of cast iron, which cannot be forged. The flasks and the bed both work green sand, which is sand blended with clay and damped so it holds an impression: 8 sand plus 1 blue clay makes 8 Green Sand.
The pattern is the specification. A Pattern carries what to cast, the station reads it off the held stack, and nothing in the station's code names a shape or a product, so another mod adds a castable part with a pattern definition alone. Patterns are carved from a reusable Diagram, pattern boards and a knife held on the Vice Bench.
The Small Flask casts capital goods, a handful at a time: iron molds, heavy plate, ladle bowls. Its loop is two clicks and a wait.
- Place the flask and right-click it once with Green Sand. The sand is rammed in and is never taken away again.
- Right-click with a Pattern. The impression is rammed up and the pattern takes a point of damage.
- Let the run fill it through the launder face, which is the face the spout is drawn on.
- Wait for it to set. An empty hand on a flask still holding liquid metal is refused.
- Right-click with an empty hand to shake it out. The part comes out, the impression is destroyed and the sand rakes back to full.
A pour that came in below the pattern's minimum temperature, full or short, hands back recovered scrap of whatever metal was in the cavity instead of the part. A pour that ran short but came in hot yields the pieces it filled and scraps the rest.
What goes wrong
A canal cell has gone solid and the chisel is refused. A cell latches solid the moment its metal drops below its melting point, but it cannot be chiselled until it is below 30% of that. For iron that is the whole span from 1482 C down to about 445 C, and during it the block reports that it is still cooling. Wait; the tool is right and the timing is not.
Metal solidified at the tap. A tap with nothing under it pours onto the ground and sets there. Put a canal start under the spout before opening a tap, or accept chiselling the plug out by hand.
A junction is filling the wrong branch. There is no routing. Every connection moves metal toward whichever side holds less, so a branch drains in whatever order the fills happen to fall in. Plate the joint of the branch that should not fill, or tap it shut.
The tap pours nothing while the canal is full. A full destination backs the run up cell by cell to the canal start, so the tap cannot push into it. The furnace keeps burning and the pool rises toward the cinder notch; drain the run before the pool gets there.
A mold on a pedestal shattered. It was fired clay and the run was above 1340 C. Iron needs an iron mold, which is what the Small Flask is for.
Metal disappeared out of a mold. It was picked up into a slot that was not the active one, or the active slot was swapped while it was still liquid.
Something poured that has no solid form. When a metal's solid drop cannot be resolved the mod hands back a block of Solidified Slag rather than destroying the charge.
Slope runners
A level run only levels, so a canal on one floor cannot carry metal down to a lower one. A slope runner does: nine slope pieces, each dropping the bed by the same small step, about 1 inch to the foot, and a drop piece as the tenth that pours into a canal start one block lower. That start roots the level canal below, so a straight, bend, tee, cross, tap or another slope joins it. A slope passes the whole stream at any length and empties when the pour stops.
Slopes place against an open connector one step at a time, each new piece continuing the last. The game refuses a slope with nothing to continue, a tenth piece with no canal start one block below it, and any other canal piece against a slope's outlet. A slope cannot be plated, so plate the level cell before it. A tap hangs on a level canal after the lower start, never on a slope.
Tested setup: four runs on one yard
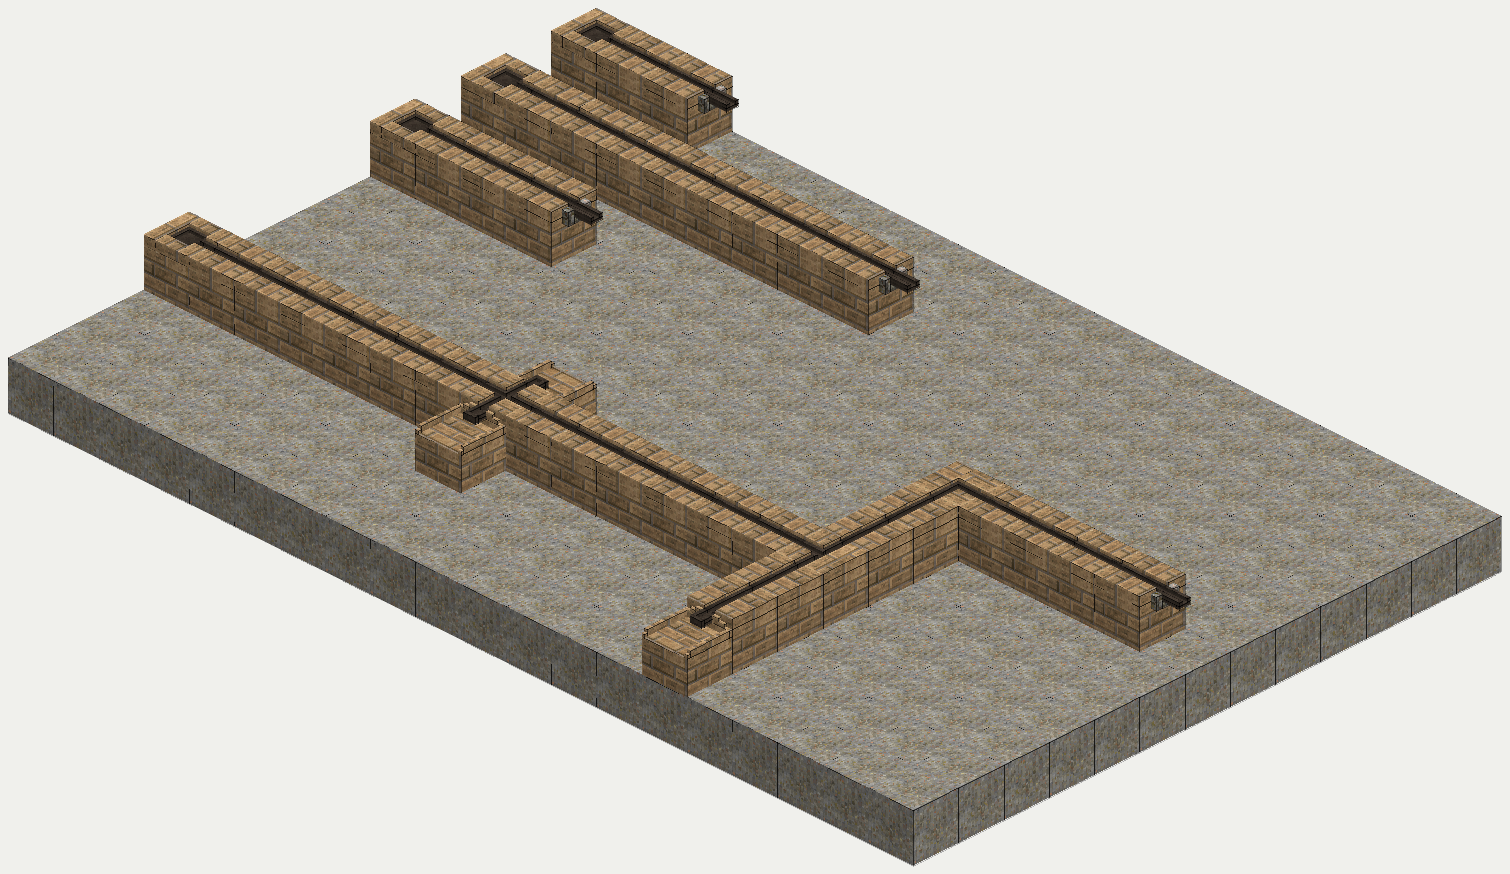
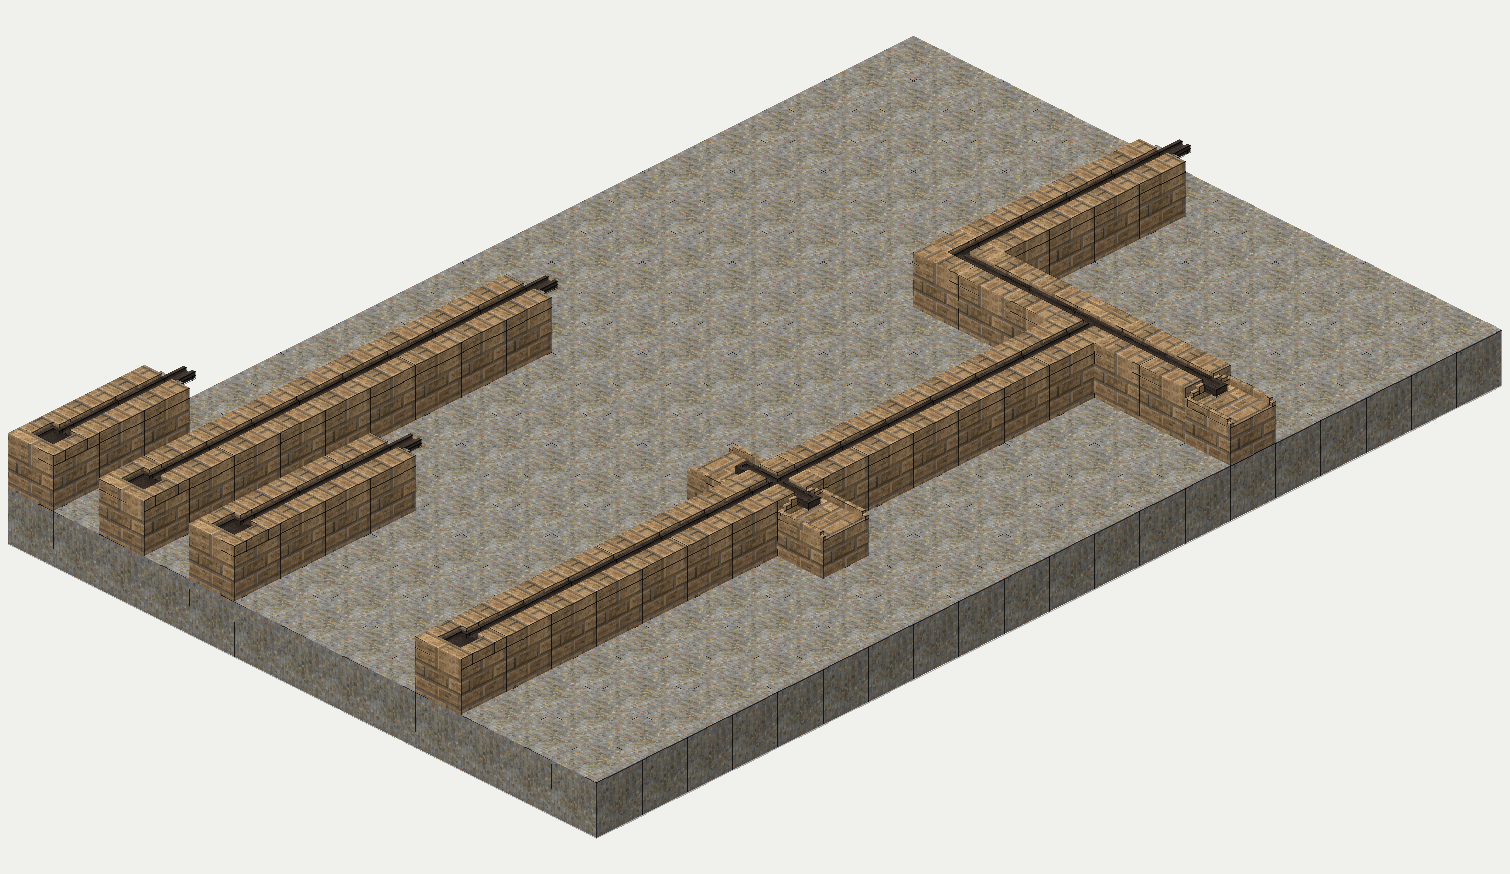
The mod's tests lay four runs side by side and pour them for five minutes, the way a player would.
- Three iron runs are laid in fire brick on granite, each a start, a row of straights and a Molten Canal (Tap) with a dried Shank Ladle parked under it: two straights in the short run, eight in the long run, and three in a run whose tap is left shut.
- The copper run is a start and twenty straights with a cross, a tee and a bend, ending in a tap with a ladle under it. Mold Pedestals stand on both arms of the cross and at the end of the tee's south arm, each with a small fired-clay axe mold.
- Ctrl plus right-click opens the taps of the short, long and copper runs.
- Iron at 1577 C goes into each iron start 40 units every ten seconds, ten times, 400 units in all. Copper at 1130 C goes into the copper start 40 units every ten seconds for the whole five minutes.
What the run shows:
- Nothing is lost: each iron run's ladle and canals together hold the 400 units poured.
- The short run leaves 20 units, the 10 unit skin of its start and first canal. The long run keeps the same skin in its start and first seven canals, 80 units, and the cell next to the tap drains empty into the ladle.
- Copper crosses the branching run as a pulse a cell a second, with no more than two empty cells behind the metal. Both arms of the cross and the tee's south arm cast their molds full, and the copper run ends with two or three of its canals set.
- The shut tap backs its run up until the start is brim full. The brim-full start takes nothing while the pour goes on, the canal beside it holds 50 units, the most one canal holds, and the ladle under the shut tap gets nothing.
The runs are placed rather than crafted. The metal goes straight into each start in place of a furnace tap, and the ladles and the molds are handed over.
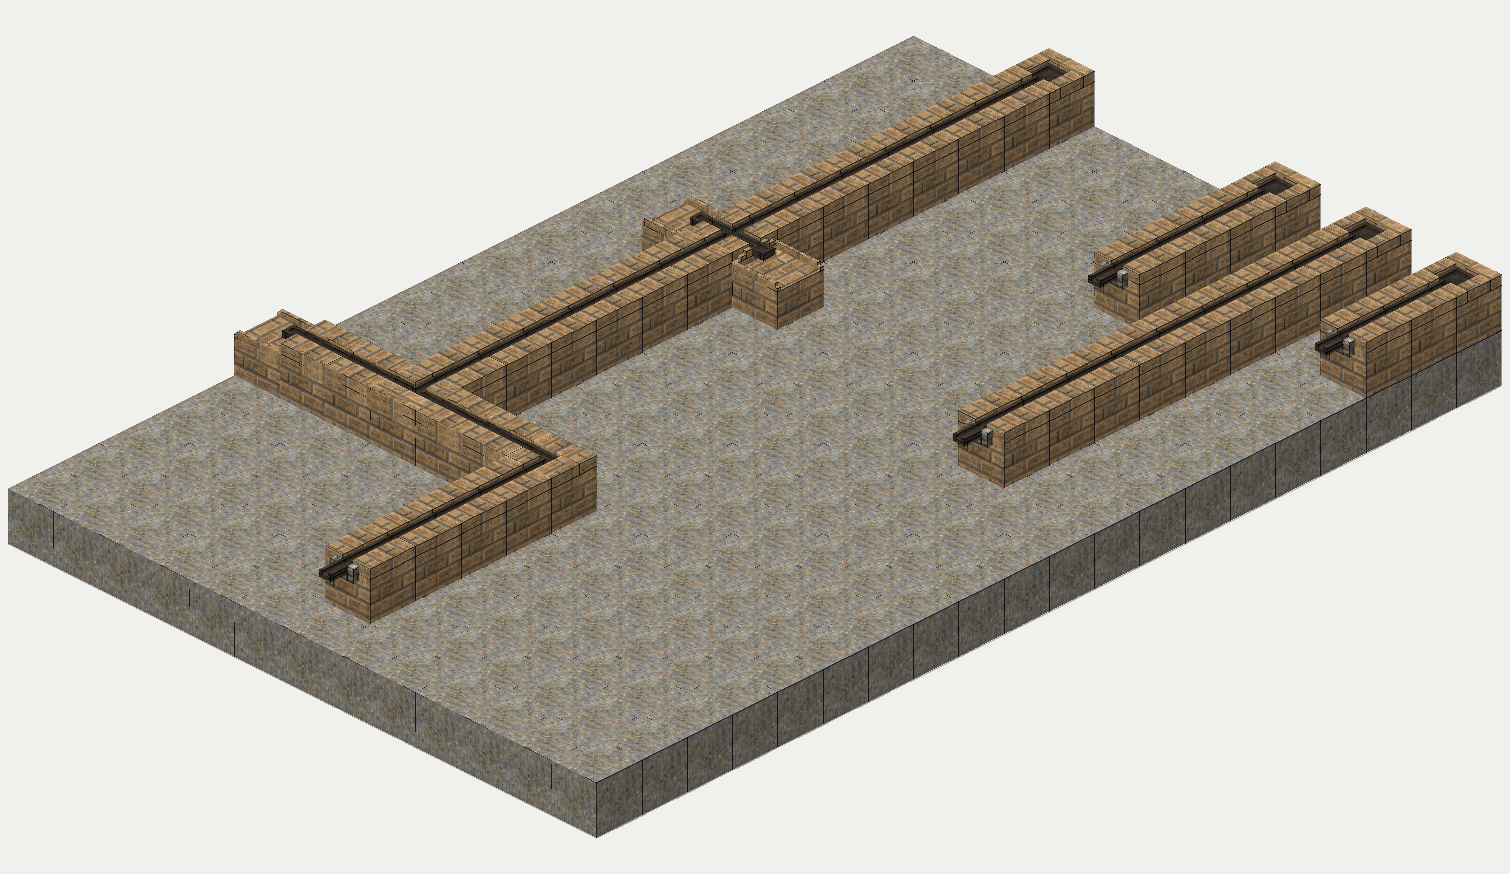
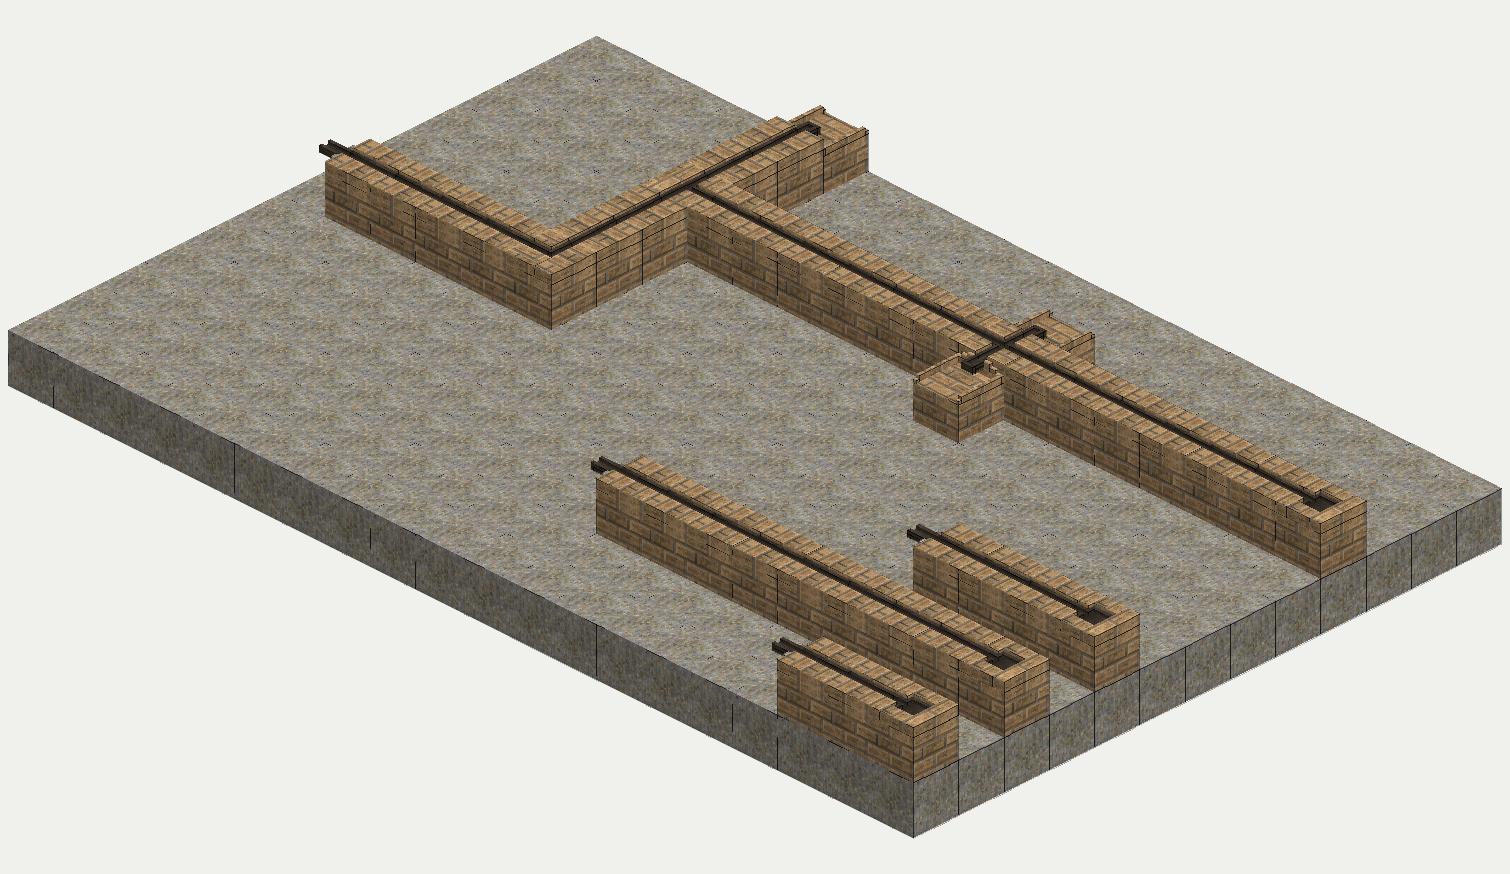
Tested setup: two metals
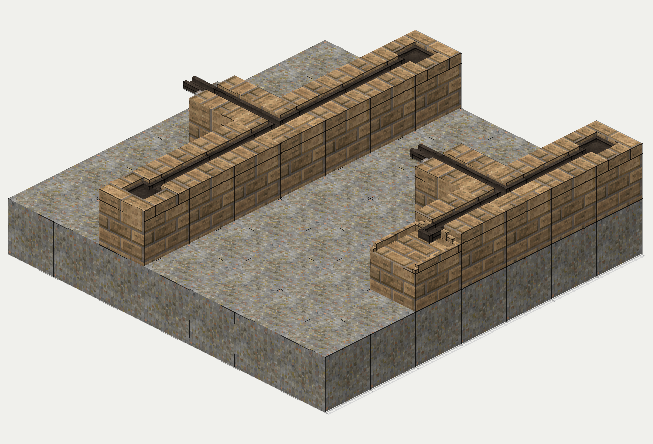
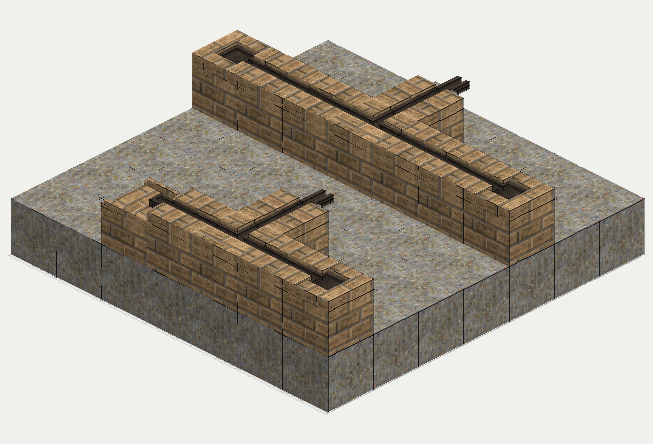
The mod's tests run copper and iron through two small plants, the way a player would.
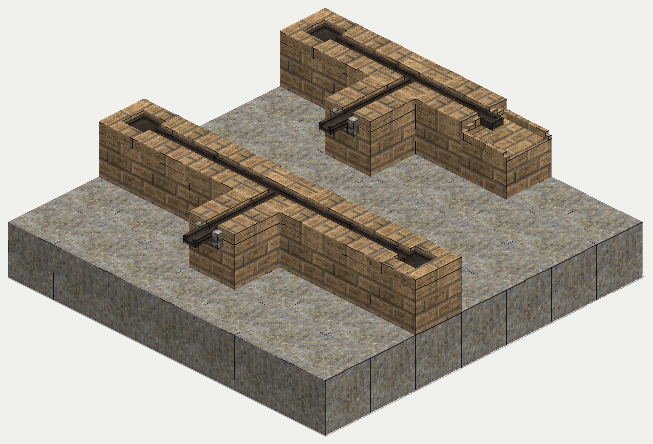
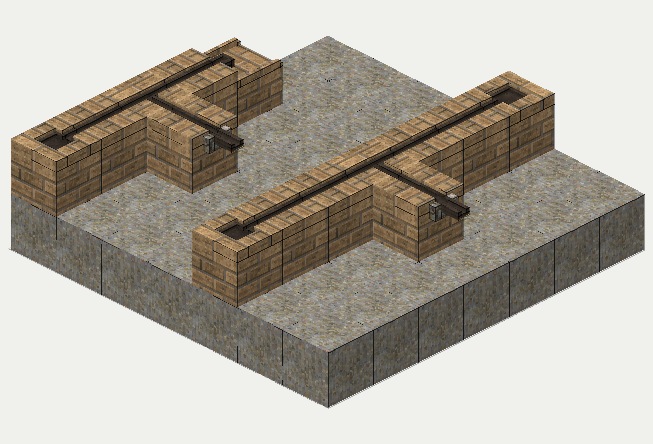
- The first plant is one fire-brick canal on granite with a start at each end: a copper start in the west, an iron start in the east, and between them two straights, a tee and two straights. The tee's branch runs one straight south to a Molten Canal (Tap) with a large fired-clay helve hammer mold parked under it, and the tap is opened.
- 120 units of copper at 1130 C and 120 units of iron at 1577 C go into the two starts at once.
- Each metal fills its own half. The tee keeps the iron that reached it first and passes it down to the tap, no cell holds both, and no copper cell takes the iron's heat: none goes above 1135 C, against the 1130 C it was poured at.
- The second plant is a start, a straight, a tee, a straight and a Mold Pedestal with a small fired-clay axe mold. The tee's branch runs one straight south to a tap with a large helve hammer mold parked under it, and the tap is left shut.
- 200 units of copper go into the start. The small mold casts 100 units and the rest stands in the run.
- Iron poured at the start while it holds copper is refused, and the start keeps its copper. The clock is moved on until the start has set, and it still refuses iron.
- The clock is moved on an hour at a time until the copper has hardened. The start, the straight, the tee and the straight down to the tap are chiselled out with the hammer in the off hand, and the tap is opened.
- 160 units of iron go into the start. The large mold casts at least 100 units of iron, and the small mold keeps its 100 units of copper.
The plants are placed rather than crafted, and the clock is moved on the way sleeping or /time add would move it. The
metal goes straight into the starts in place of a furnace tap or a crucible, and the molds, the chisel and the hammer
are handed over.
Tested setup: spilling on an iron floor
The mod's tests spill three molds, the way a player would, to show where the metal lands.
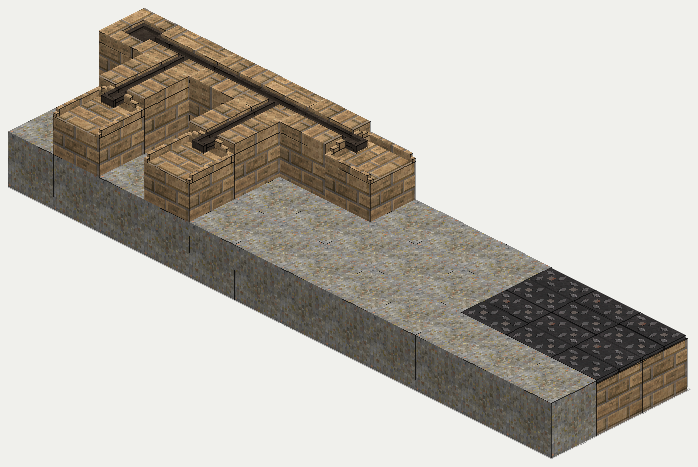
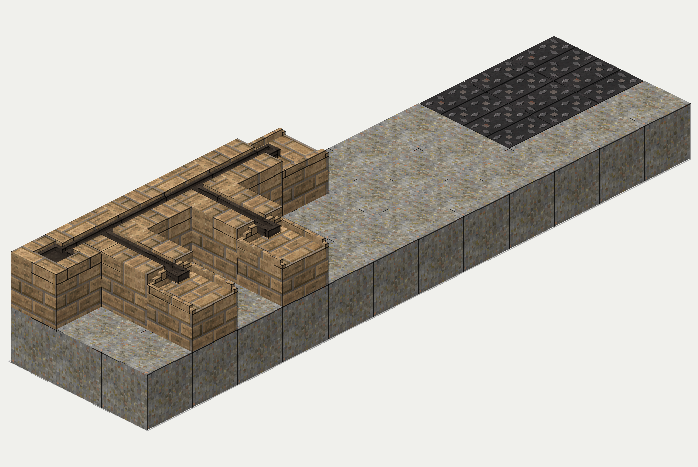
- A fire-brick canal is laid on granite: a start and four straights to a Mold Pedestal at the east end, and from the first and third straights a branch of one straight south to a pedestal each. Six cells of iron floor are set into the ground a few blocks east of the canal.
- A small fired-clay axe mold parks on each pedestal, and 360 units of copper at 1130 C go into the start, 40 at a time over nine seconds.
- The first branch's mold, full, is lifted into an empty hand. Standing on the iron floor, moving to another hotbar slot spills it, and the metal lands as a puddle in that one cell.
- The second branch's mold, full, is spilled on the same spot. That cell is already full, so the rest spreads to the next floor cell east and nowhere else.
- The east pedestal's mold is lifted half full and still liquid and spilled standing beside the floor, not on it. That metal lands nowhere.
- An hour later both puddles have hardened. Chiselled out with the hammer in the off hand, they give 30 copper bits, three quarters of the 200 units spilled. The third mold goes back on its pedestal empty.
The canal and the floor are placed rather than crafted, and the clock is moved on the way sleeping or /time add
would move it. The copper goes straight into the start in place of a furnace tap or a crucible, the molds, the chisel
and the hammer are handed over, and the server has EnhanceVanillaMolds turned on so the vanilla molds can be lifted
full and can spill. Spilled metal is set to cool fifty times faster than the game's default, so the puddles harden
within that hour.
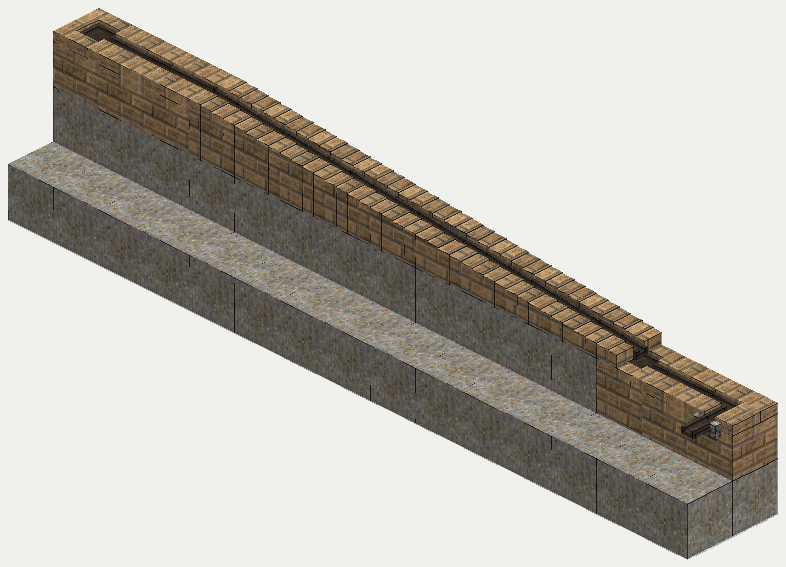
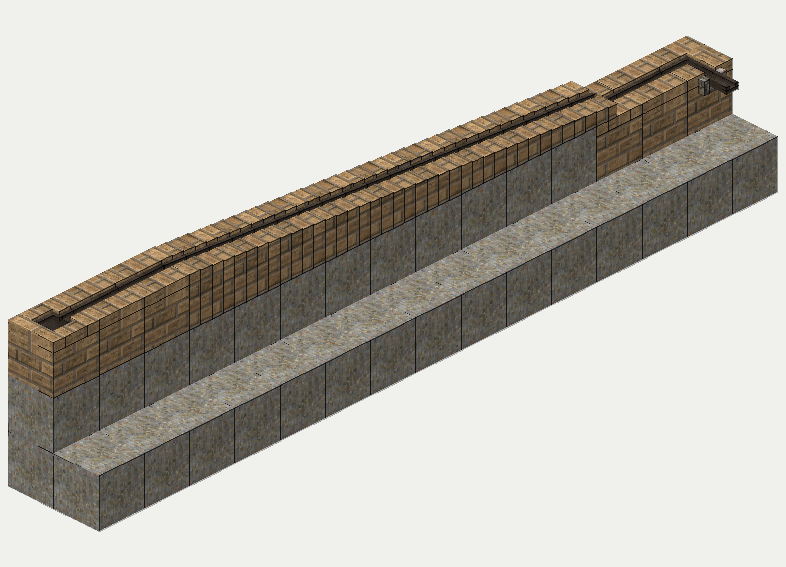
Tested setup: a slope runner down one floor
The mod's tests lay this runner and pour iron down it, the way a player would.
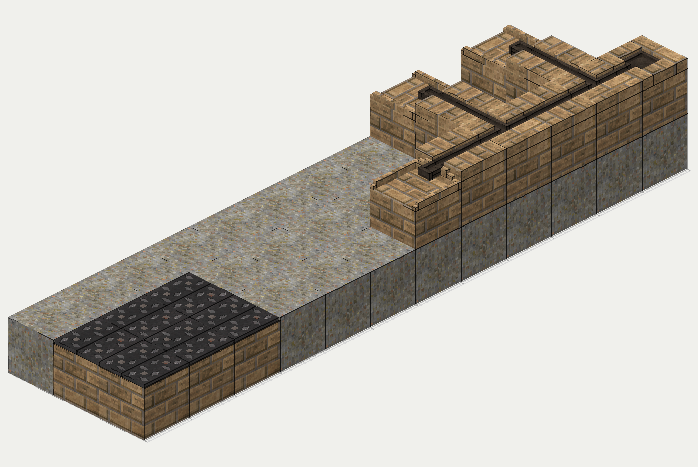
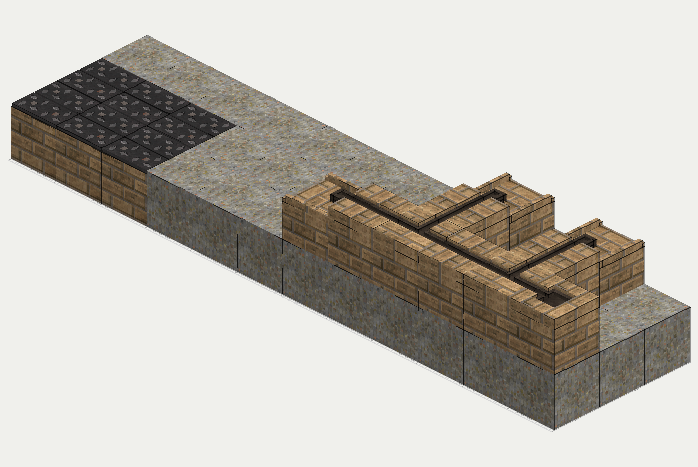
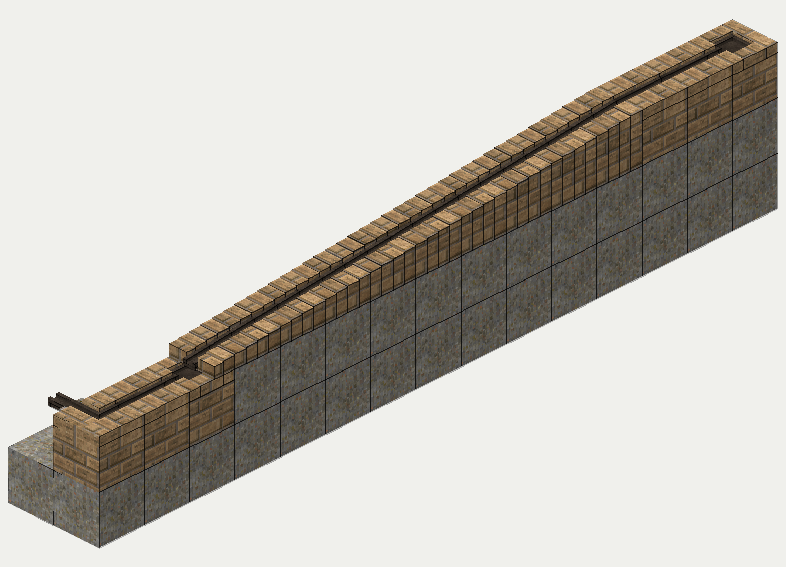
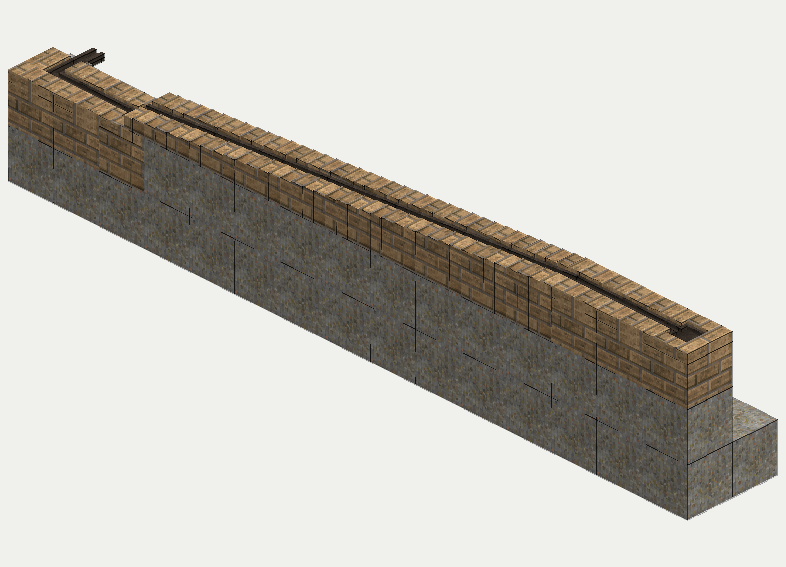
- On granite piers a block high, a Molten Canal (Start) and two straight pieces run east.
- Nine slope pieces follow, each one step lower than the last, and the Molten Canal (Slope Drop) as the tenth.
- One block lower, a second Molten Canal (Start) sits under the drop's lip, and a straight piece and a bend lead from it to a closed Molten Canal (Tap).
- Three pours of molten iron, 40 units each at 1577 C, enter the start 10 seconds apart.
- The iron runs down. The two level cells before the slope keep their 10 unit skin, the slope pieces and the drop stand empty once the pour has passed, and 100 of the 120 units stand in the lower start and the level canal after it. The closed tap takes none.
Molten metal cools at 1 C a second in this run instead of the usual 24, so the iron stays liquid along all fifteen cells. The piers are granite where a player would lay stone or brick, the slope pieces are set to their steps rather than placed one against the next, and the iron is poured straight into the start in place of a furnace tapping into it.
Planned
This section is planned and not yet in the game; until it lands, the rules above apply.
The bottom-pour ladle
A ladle will hold metal between a run and the mold, and it pours from the bottom as period casting ladles did: a stopper rod lifts off a fire-clay nozzle in the vessel's floor and a vertical stream falls from beneath the slag into the canal start under it. It does not tilt. The vessel is an octagon 2.5 blocks across in a 3 x 3 footprint, three blocks tall, and holds about 29,700 units, roughly 46 times a cupola hearth. The size is set by the runners: a launder reaches only a little past its own cell, so the bath is made wide enough that each runner's end stands over it.
The ladle comes in two builds. The plate ladle is hammered iron plate, so it does not wait on the rolling mill; the cast ladle takes the ladle's own casting, which is cheaper per unit and saves plate. The vessel is lined with tier 1 refractory brick, because fired clay is capped at 1200 C and the metal it holds melts above that.
It is built in stages: two cast-iron standards, the shell, the lining, the nozzle and stopper, and the lever. The standards stand north and south of the outlet cell and carry the vessel on lugs; it never turns on them. The stopper is worked by hand. Right-clicking the lever opens the stopper and the next click shuts it, and while it is open the ladle pours at 44 units per second into the outlet cell. The outlet cell is left free: the player places a canal start there as an ordinary block, turned toward the side the run leaves by.
::shape{file="shapes-finished/molten/ladle/molten-megablock-laddle-proposed.json" views="iso" anim="poursouth" title="The bottom-pour ladle on its standards"}
Supports and the outlet side
Metal comes in on up to three sides, every face except the lever's, and only at the rim's level, two blocks above the outlet. The ladle therefore stands in a pit, or the runners come from taps raised two blocks; either way it drops a flow two levels.
Each input is a support: a cast-iron trestle standing just outside the ladle's footprint and carrying a launder, a fire-clay-lined cast trough. A support is built in three stages: the trestle, the launder and the fire-clay lining of its groove. The player holds the support's first-stage item and right-clicks any ladle cell on the side wanted. The ladle draws from each attached launder at 25 units per tick. A support is refused on the lever side, on a column with anything in it or nothing solid under it, on a side that already has one, and on the side the outlet canal leaves from. The outlet canal and a support never share a side, and an outlet canal refuses a side that holds a support. A support cannot be placed except through a ladle; its only connector is its outer face, where an incoming canal joins the launder.