
Furnaces and heat
as of 0.8.0
No furnace in this mod has a maximum temperature. Each one settles where the heat it makes and the heat it loses balance, and both sides of that ledger are on the block info. A furnace that stalls short of its melting point reads as a number, not as a mystery.
The two families
| Family | Furnaces | Fire | State |
|---|---|---|---|
| shaft | Cold blast furnace, Cupola furnace | a raceway in front of the tuyeres, blown under pressure | derived every tick from the charge; no timers |
| reverberatory | Puddling furnace, Heating furnace, Crucible furnace | a Firebox bed, drawn by the stack | stored, with soak and burn timers |
| retort | Coke oven | none of its own: the sealed charge bakes once a flame lights it at the door | stored, with a soak and then a clock for the chamber |
A shaft furnace burns a column of charge from the bottom. A reverberatory furnace burns a fuel bed beside the work and carries the flame over a bridge to it, so the fuel never touches the metal.
The law
T_process = max(ambient, T_in - T_loss)
Heat in:
fuelFactor = clamp(1 + 0.35 * (fuelFrac - 0.20) / 0.20, 0.35, 1.25)
airFactor  = 0.5 + 0.5 * clamp(blastSupply, 0, 1)
T_in       = 950 + 900 * fuelFactor * airFactor + 0.35 * max(0, blastTemp - ambient)
Heat out:
T_loss = 120 + chargeLoss + 1.0 * max(0, 20 - ambient)
fuelFrac is the carbon fraction of what stands in the shaft, not a volume fraction of coke: coke
counts 1.0 per unit and charcoal 0.5, so how the rounds are laid is the one dial. airFactor is 0.5
with no blast and 1.0 at full supply, and it multiplies the coke gain, so losing the blower costs
450 C at the reference burden rather than a proportional slice. The preheat term needs blast hotter
than ambient, which only a charged cowper stove supplies; there is none in this mod, so every
furnace here runs cold blast and that term is zero.
chargeLoss is linear in how full the furnace is, which inverts the obvious intuition: topping a
marginal furnace up makes it colder, and a thin charge runs hotter and exhausts sooner.
| Machine | Charge loss at full | Transfer loss over the bridge |
|---|---|---|
| shaft furnace | 310 C | none |
| reverberatory hearth | 100 C | 100 C |
| crucible hearth | 50 C | none, the pots stand in the fire |
What a cold blast furnace reaches
Full hearth, 20 C ambient, full blast supply, so T_loss is 430 C. Iron melts at 1482 C.
| Burden carbon | fuelFactor | T_in | T_process | Melts iron |
|---|---|---|---|---|
| 10 per cent | 0.825 | 1692.5 C | 1262.5 C | no |
| 20 per cent | 1.000 | 1850.0 C | 1420.0 C | no |
| 30 per cent | 1.175 | 2007.5 C | 1577.5 C | yes |
| 34.3 per cent or richer | 1.250 (capped) | 2075.0 C | 1645.0 C | yes |
| 20 per cent, blowers off | 1.000 | 1400.0 C | 970.0 C | no |
Break-even on cold blast at a full shaft is 23.94 per cent carbon. A cold blast furnace therefore wants a richer charge than the 20 per cent reference, and pays for it in fuel. Running lean is what the steam tier is for.
A half-full shaft pays half the charge loss, so T_loss falls to 275 C and a 20 per cent charge
settles at 1575 C and melts. That is the other lever, and it costs campaign length.
The Cupola furnace melts cast iron at 1200 C, which a plain 20 per cent charge clears by 220 C on cold blast. Remelting scrap is an iron-age job; reducing ore is not.
Melt speed
factor = clamp(1 + 0.75 * (T - meltPoint) / 200, 0.5, 2.0)
Superheat buys speed on both families. A shaft furnace has no melt cycle to wait out, so the factor multiplies the burden it renders per second; a firebox furnace fires its melt cycle every 10 seconds divided by the factor. There is no second yield constant anywhere: a hotter furnace makes more iron from the same carbon.
Blast: what the burden demands
Neither the pressure a furnace needs nor the air it draws is a property of the machine. Both come out of the burden's carbon fraction, and they move in opposite directions, because the fuel layers are the permeable skeleton the blast gets through. The pressure is a threshold and not a target: a line standing below it is not drawn on at all, however much air it holds.
pressure  = clamp(2.0 + (0.20 - fuelFrac) * 7.5, 1.2, 6.0) atm
draw      = 14 * clamp(fuelFrac / 0.20, 0.4, 1.8) L/s per tuyere
Cold blast furnace, two tuyeres:
| Burden carbon | Pressure demanded | Draw per tuyere | Draw total |
|---|---|---|---|
| 10 per cent | 2.75 atm | 7.0 L/s | 14.0 L/s |
| 20 per cent | 2.00 atm | 14.0 L/s | 28.0 L/s |
| 30 per cent | 1.25 atm | 21.0 L/s | 42.0 L/s |
| 36 per cent or richer | 1.20 atm | 25.2 L/s | 50.4 L/s |
The Cupola furnace draws 12 L/s through each of its two tuyeres at the reference fraction and asks the same pressure.
The air comes from a Tub Blast Machine, which is the tier's only air source and needs nothing but an axle: a vanilla waterwheel or windmill runs it. It delivers 45 L/s at an axle speed of 0.45 or above, nothing at 0.15 or below, and raises the line to at most 2.2 atm. That ceiling is the tier gate. A 30 per cent burden asks 1.25 atm and blows easily; a 10 per cent burden asks 2.75 atm, which is above the blower's ceiling and above what Plated Piping (Straight) will hold. See Pipe networks and pressure.
Blast supply is arrived air over demanded air, and it is a cliff rather than a slope. A tuyere draws nothing unless the line at it stands at or above the pressure the burden demands, so a main a tenth of an atmosphere short delivers no air at all: supply reads zero, the air factor sits at 0.5 and the furnace runs exactly as though nothing were piped to it. There is no partial credit for being close, and raising the line to the demanded pressure is the whole of blowing a furnace in.
A lit furnace that needs blast and gets under 0.1 of its demand flags air-starved on its block info. On a shaft furnace that is a readout and nothing else: the fire goes on burning at natural draught.
Natural draught: the stack
A reverberatory furnace has no blower. Its air factor comes from its chimney instead:
airFactor = 0.5 + 0.11 * sqrt(courses) - 0.00102 * courses^2
then multiplied by 0.35 if the Chimney Damper is shut and by 0.6 if a Charge Door is open and spilling the pull into the room. A course is one air cell ringed by brick on all four sides. The curve peaks at 9 courses and declines past it: a stack built too tall makes the furnace worse rather than merely no better, and the block info names both the count standing and the count it is rated at.
Every reverberatory furnace but the Crucible furnace has its stack fixed by its own layout. The crucible furnace counts what the player built on top of its flue, which is what makes its chimney its temperature dial.
Refractory tier
Shaft furnaces and the two reverberatory hearths are laid in refractory bricks of any tier. The core takes the tier it was crafted from and wears its texture; the layout accepts any tier in the walls. Tier is appearance, not a rating. The Coke oven is ordinary fire brick throughout, deliberately, because everything downstream waits on it.
Lighting and going out
A shaft furnace is blown in through a tap. A newly built Iron Tap or Slag Tap comes plugged. An empty hand on a plugged tap breaks the plug out; a flame held against an open tap reaches in and lights the charge; 4 fire clay on an open tap stops it again. Breaking a plug refunds nothing, so blowing a furnace in costs one clay plug each time.
Ignition is positional and has nothing to do with the blast: carbon has to stand at the raceway of every column, and a flame held through an open tap lights it whatever the blowers are doing. Air is what carries a lit furnace to a melting point, not what lights it. A furnace with no blast at all burns on at an air factor of 0.5, which is natural draught. A firebox furnace needs no flame: it lights itself when its beds are full.
Shaft state is derived every tick, with nothing stored:
| Reported | Means |
|---|---|
| Idle | not lit, or no carbon left at the raceway |
| Firing | burning, but the burden at the raceway is not at its melting point, or the charge is not something the furnace converts |
| Melting | burning and rendering metal |
A furnace can run Firing for a whole campaign and make nothing. That is the chill: a cold band stops its column, everything above rests on it, and a hung column never brings fresh carbon down, so a chilled furnace goes out within minutes on its own. The recovery route is to break the charge blocks out of the shaft.
Reverberatory furnaces (puddling, reheating, crucible) derive their state the same way:
| Reported | Means |
|---|---|
| Idle | not lit, or every bed empty |
| Firing | lit, whatever the chamber temperature |
| Melting | never shown on these furnaces |
A bed holding any fuel is lit by hand, with a torch or a firestarter held on it (shift and right-click, as on a coal pile), and from then on every bed burns 1.2 units a game hour whatever the heat, so a full bed lasts 10 game hours. Whether the work is at heat is read from the chamber temperature against the furnace's line each tick, not from the label. Charge a course into a lit bed before the last one drops to keep the fire going; a bed that has gone out is lit by hand again, though one charged while the chamber is still hot catches from the heat left.
A furnace whose beds are spent does not lose its heat at once. The chamber cools toward ambient at 480 C a game hour, the work follows the falling heat (a reheat soak stops once it is under 900 C, a puddling bath freezes as the chamber drops under 1400 C, crucible pots keep melting until it drops under 1600 C), and a furnace relit before it is cold starts from the heat left, never under 900 C.
Tapping
A shaft furnace keeps its products as one pool on the crucible floor, level across every pool cell, iron below and slag floating on it. The hearth bottom is sand up to the iron tap's channel, the slag notch sits 10 voxel layers over the floor of the crucible course and the tuyeres 16. A layer holds 640 u in each pool cell, so the Cold blast furnace, with three pool cells, holds about 15 000 units of iron under its slag notch, and the Cupola furnace, with one, about 5 000. Melting never stalls on the pool; it rises while the furnace burns. Tap before the iron reaches the slag notch: iron that gets there runs out of the slag tap, plugged or open, and sets in the runner head as a lump that chokes the tap until it is broken out with a pickaxe. A pool that rises to the tuyeres floods them and puts the furnace out; the pool then cools where it stands and an open tap still drains it.
An open tap pours continuously; there is no separate pour toggle. The iron notch sits at the crucible floor and drains the metal, the slag notch sits higher in the same wall and skims what floats. A tap considers 50 units of pool per tick and passes 0.6 of them at the iron notch and 0.8 at the cinder notch, slag being thinner. The iron tap draws the iron off the bottom and, once none is left, the slag above it, so a tap left open empties the hearth; the slag tap draws only the slag standing above its notch. On coke the blast furnace makes about 1.8 units of iron to 1 of slag, so the slag reaches the cinder notch before the iron does and runs off there before the iron is cast.
The pool shows in each pool cell as a Hearth Pool block, liquid or set. Liquid refuses an ordinary break; set metal and slag break out with a crowbar or chisel, a stack at a time.
With a canal start under the spout the metal runs off to be cast. With nothing under it, the metal solidifies at the tap and is chiselled free by hand.
What goes wrong
The furnace is lit and the temperature will not climb. Read the ledger on the block info. Either the charge is too lean, in which case the fix is richer rounds, or the blast supply is short, in which case the fix is the blower or the pipe.
The blast line will not hold pressure. An open pipe end vents to atmosphere, and a leaking run is clamped to 1 atm no matter how hard it is blown. Cap every end against a port, a valve or an outlet.
A reverberatory furnace went out on its own. Its beds burnt down, at 1.2 units a game hour each, or were raked empty. Charge the Firebox before the last course drops, and light it again with a torch or a firestarter, or charge it while the chamber is still hot.
The temperature is right and nothing is being made. The state says Firing, not Melting. Either the raceway's burden band is below the melting point, or the shaft holds charge the furnace does not convert, such as ore burden in a cupola, which burns, counts toward fullness and renders nothing.
A wall was knocked out and the furnace will not re-light. A breach vents the blast, so the furnace drops to natural draught while it is lit and refuses to light again once it is out. Complete the structure before putting a flame to it.
Iron came out of the slag tap. The iron rose to the cinder notch. Tap the iron earlier, and break the lump out of the runner head before the slag tap will pour again.
The puddling furnace's fire hole
The puddling furnace's stoking door is replaced by a cast plate with a small square hole in it, a shovel's width, and a ledge before the hole. There is no door to open: coal piled on the ledge closes the hole, and the coal lies there while the firebox holds fuel. Behind the plate a grate on a dead plate, the fireplace, carries the coal, so the fuel level can be read through the hole. The fireplace holds 9 units and the furnace's firebox 12, so the furnace holds 21. The two beds share one burn: the furnace burns 1.2 units an hour from the fuller bed, the same as before the plate. The plate serves the puddling furnace only; the heating furnace keeps its door, and the Crucible furnace keeps its door, which is its damper.
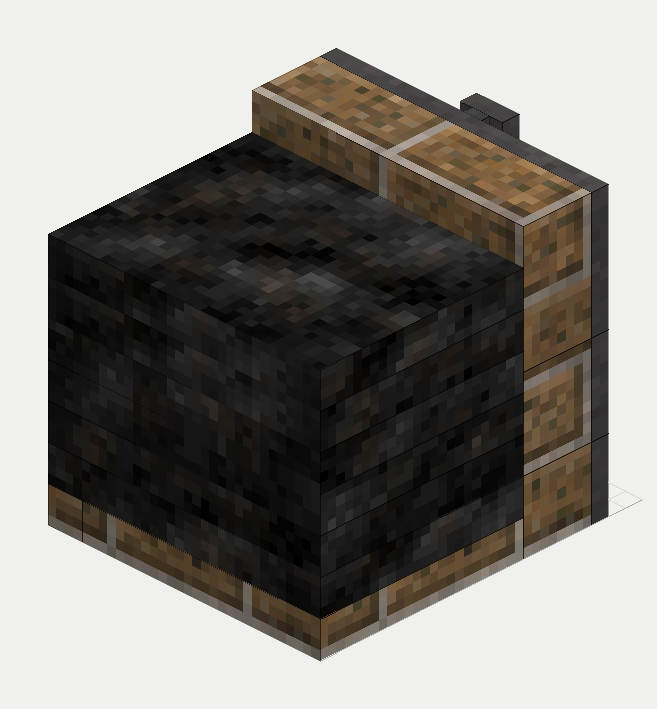
Planned
This section is planned and not yet in the game; until it lands, the rules above apply.
The puddling furnace's damper
The chimney cap is redrawn as a lever damper. A cast bracket on the stack carries a cranked lever; a flat plate on the stack top hangs from the lever's short arm, and the long arm reaches out past the stack to an eye. A rod runs from the eye down the stack face to a pull at hand height, a chain to a catch about 1.5 blocks up. The damper works as before: shut it scales the draught down and open it lets the stack pull, and the pull is how it is thrown. To open it, lift the ring off the upper pin, swing it out and hook it on the lower.
Doors on chains
The puddling furnace's charge door is a cast box lined with fire brick, hung on a forged link chain from a lever on a post over the front wall, balanced by a counterweight on the lever's short arm. The door lifts straight up in its frame. Open, it leaves the opening clear to reach through and walk past; shut, it closes it. Each door takes a length of forged chain in its recipe.
The heating furnace's two leaves
The heating furnace gets a door of its own, three cells wide, in two leaves of one and a half cells each, side by side in one cast-iron frame, meeting on rebated stiles with a guide between them. Each leaf is a wrought-iron box filled with fire brick, with no draught holes, and hangs on its own chain from its own lever over the front wall; the lever's short arm carries a cast counterpoise, and the recipe takes two chains. Each leaf lifts 11 voxels on its own. An open leaf leaves the opening under it clear to reach and walk through; shut, it closes it.
The two leaves exist for the stock, which lies in three rows across the hearth. A slab laid lengthwise passes through the leaf over its own row: the west row needs the west leaf up, the east row the east leaf, and the centre row needs both. A piece laid crosswise needs both up. The cast slab and the wider stages do not fit through a one-cell door, and a long piece laid crosswise cannot enter the hearth end first through any single door.
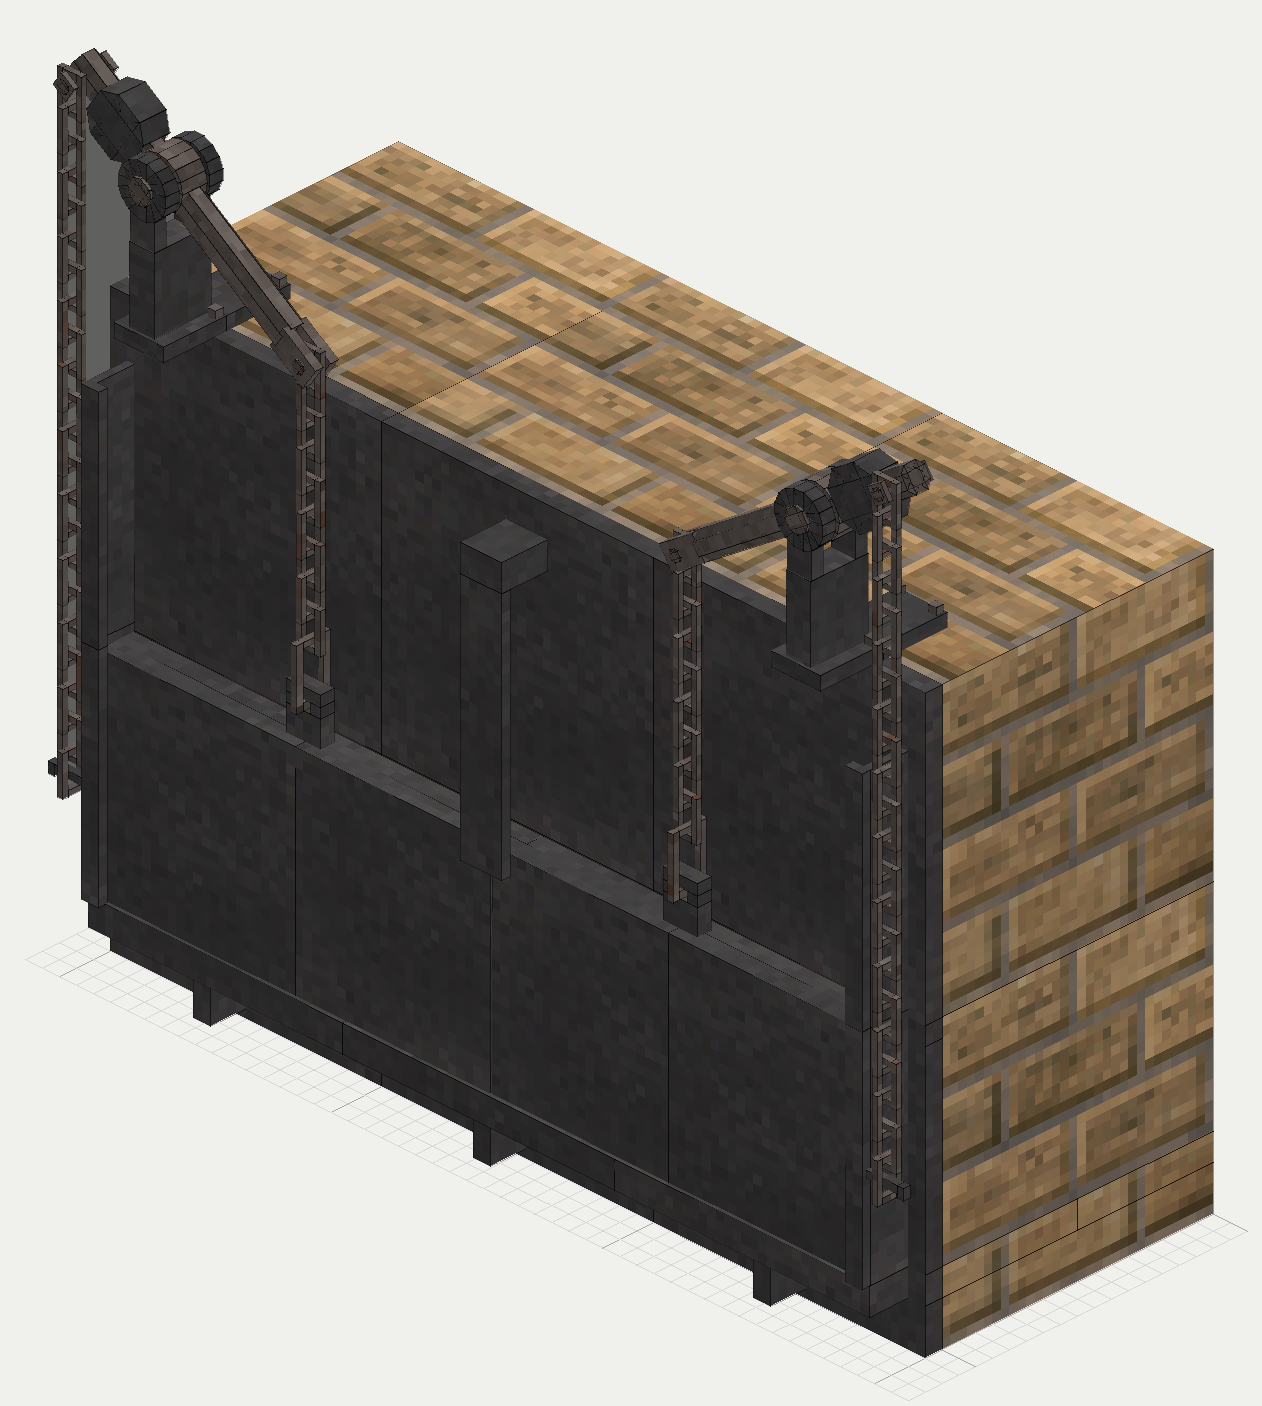

Two blowers
A shaft furnace is blown by one of two machines, and each ends in a main of its own tier. See Pipe networks and pressure for the mains.
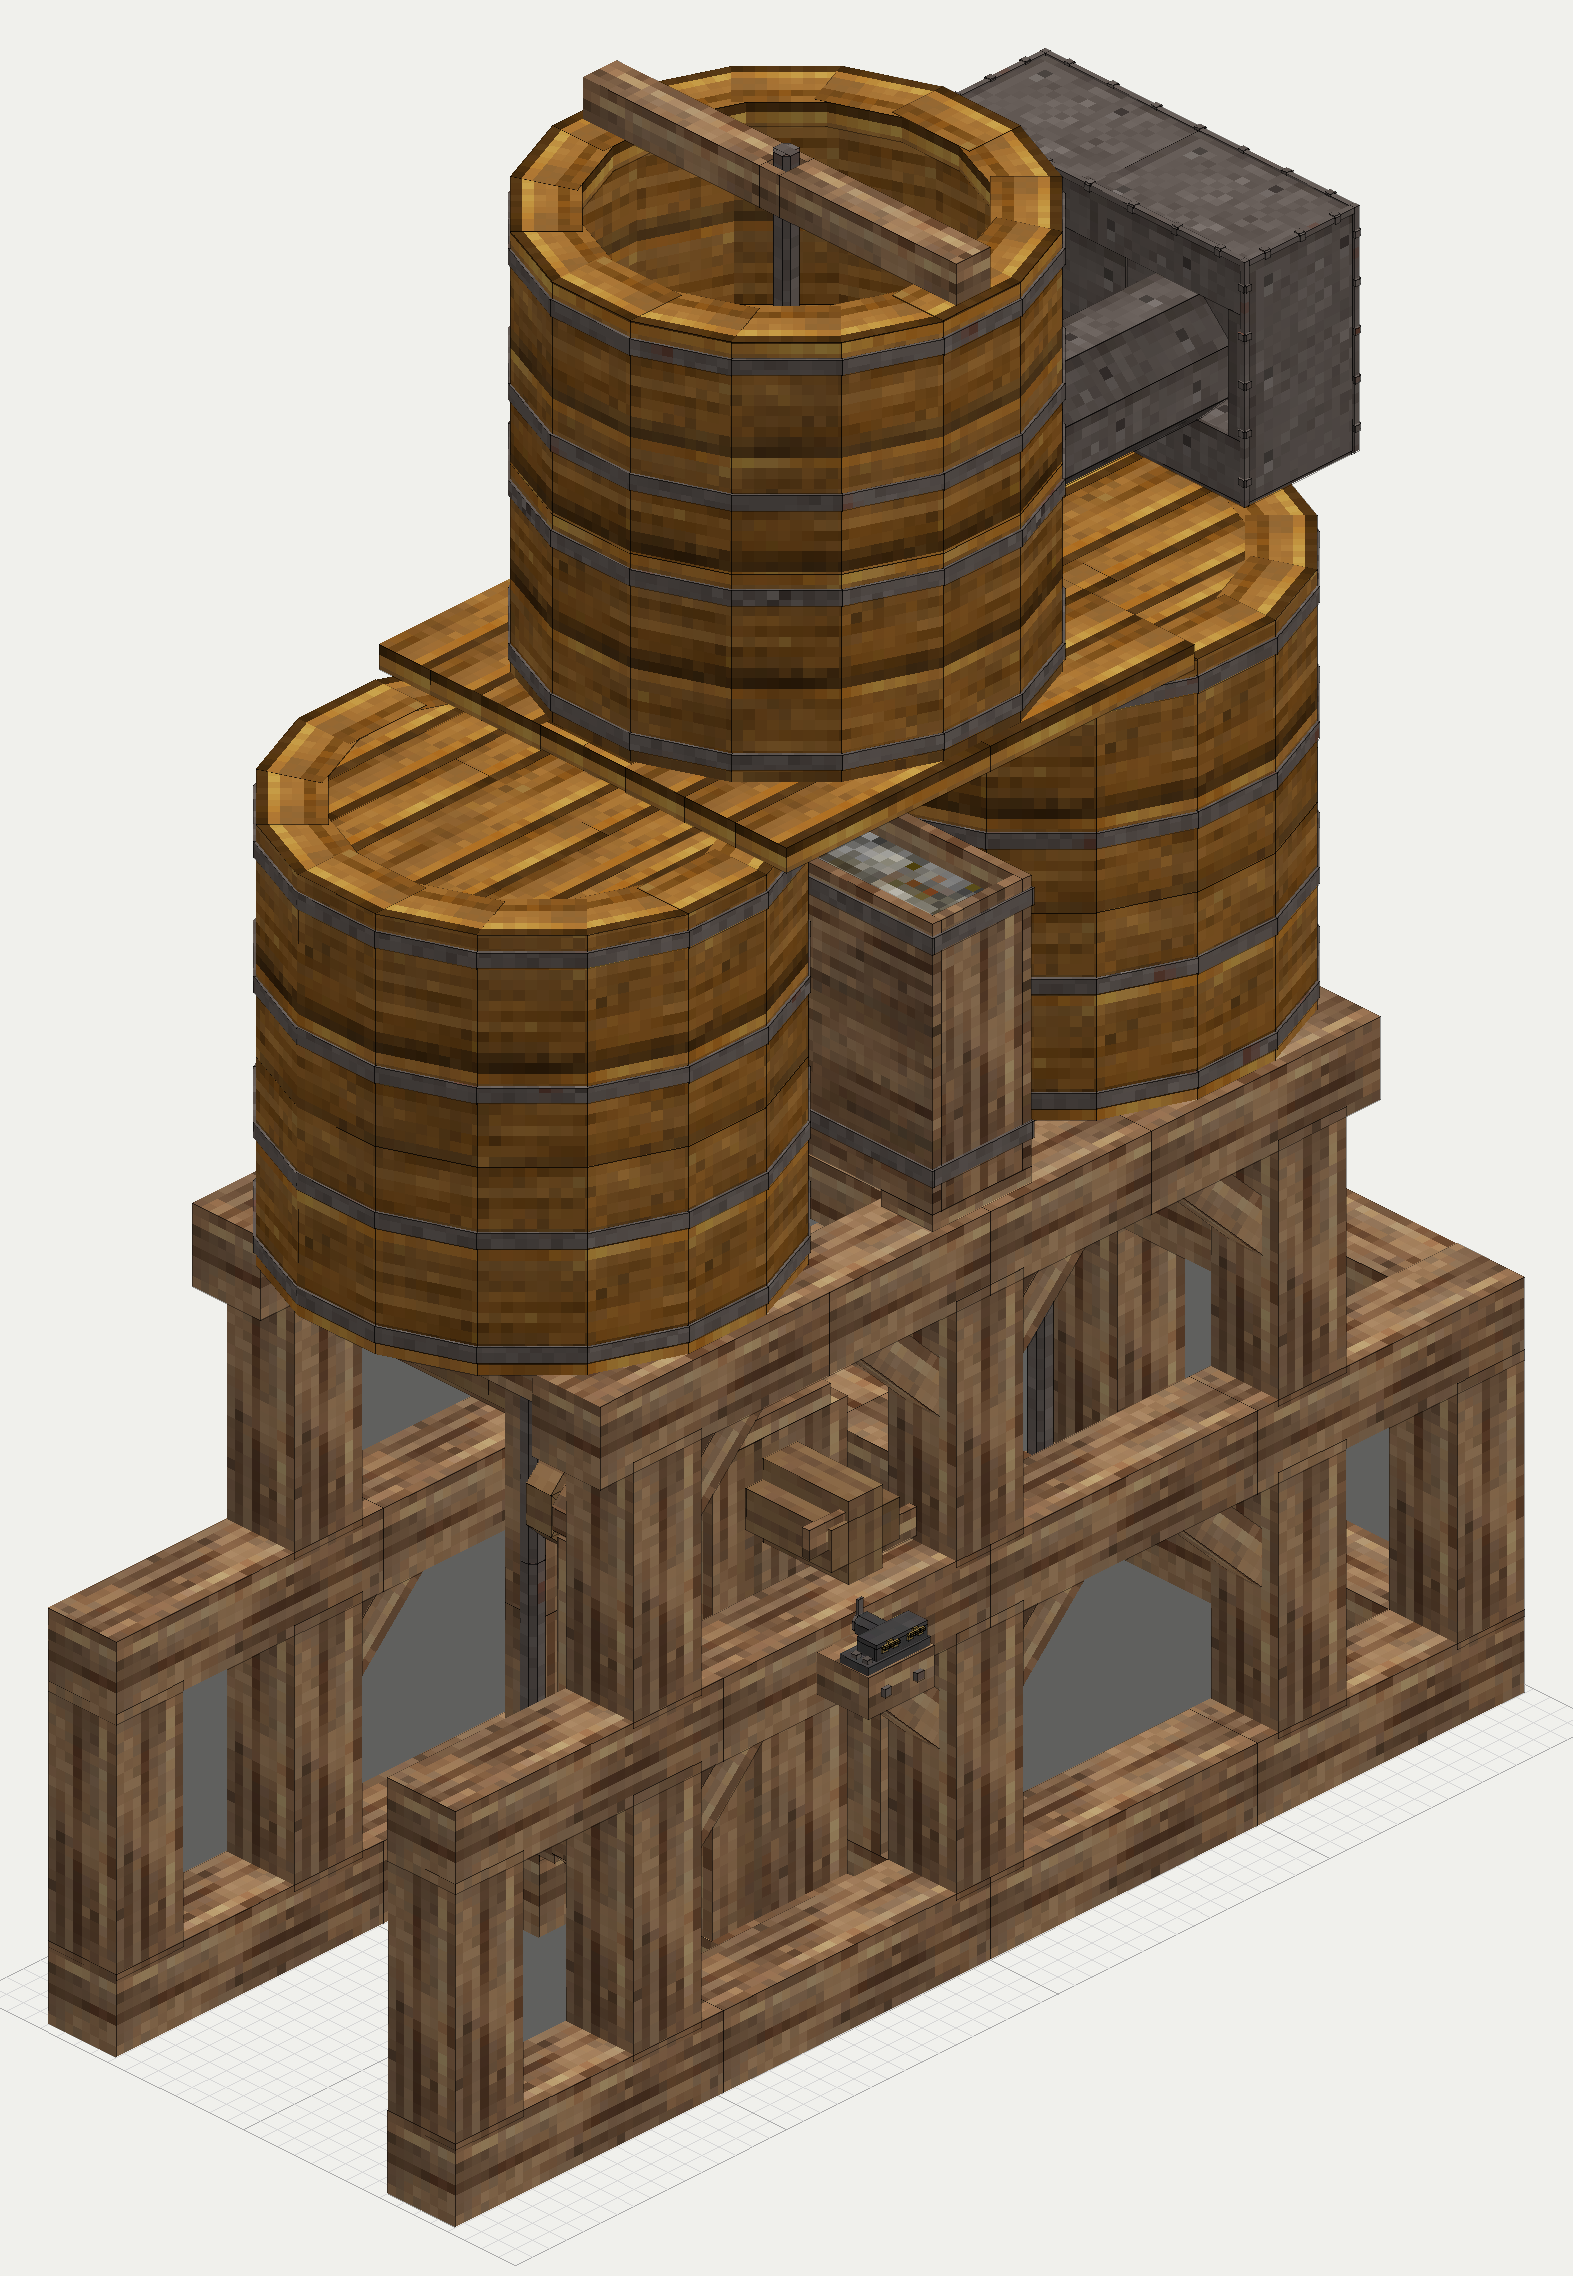
The Tub Blast Machine stays the first blower, wood and wrought iron with no cast iron in it. Its oak frame carries two tubs of glued wooden segments under iron hoops, and a receiver beside them. A wooden crank on the vanilla axle works an oak beam that rocks about 20 degrees each way, and the beam works the two tub pistons in opposition, one rising as the other falls. Each piston has leather leaves that open as it falls and the receiver has delivery flaps that open as it rises. A weighted regulator piston on the receiver lifts as the pressure rises. The blast leaves through a bolted plate air box into a plated main on the machine's north face, and the axle enters on its west face, turning in two plank stands.

The Cylinder Blast Machine is its cast counterpart, driven from the iron shafting rather than the vanilla axle. A cast horizontal cylinder is double-acting: a piston on a rod through both heads blows from each end in turn. Each head has two flaps of leather-lined sheet iron that hang shut by their weight, the inlet opening inward as that end draws and the delivery opening outward as it blows. A pinion on the main shaft drives a spur at 2:1 down onto a crank, so the crank turns at half the shaft's speed, and a connecting rod and crosshead work the piston. Each stroke sweeps 78 L, and a crank turn makes two. Both deliveries run into a riveted air chamber, 235 L, that evens the pulses before the blast leaves through a cast main. Being cast, it is the blower for the cast main and the iron shafting, as the tub machine is for the plated main.
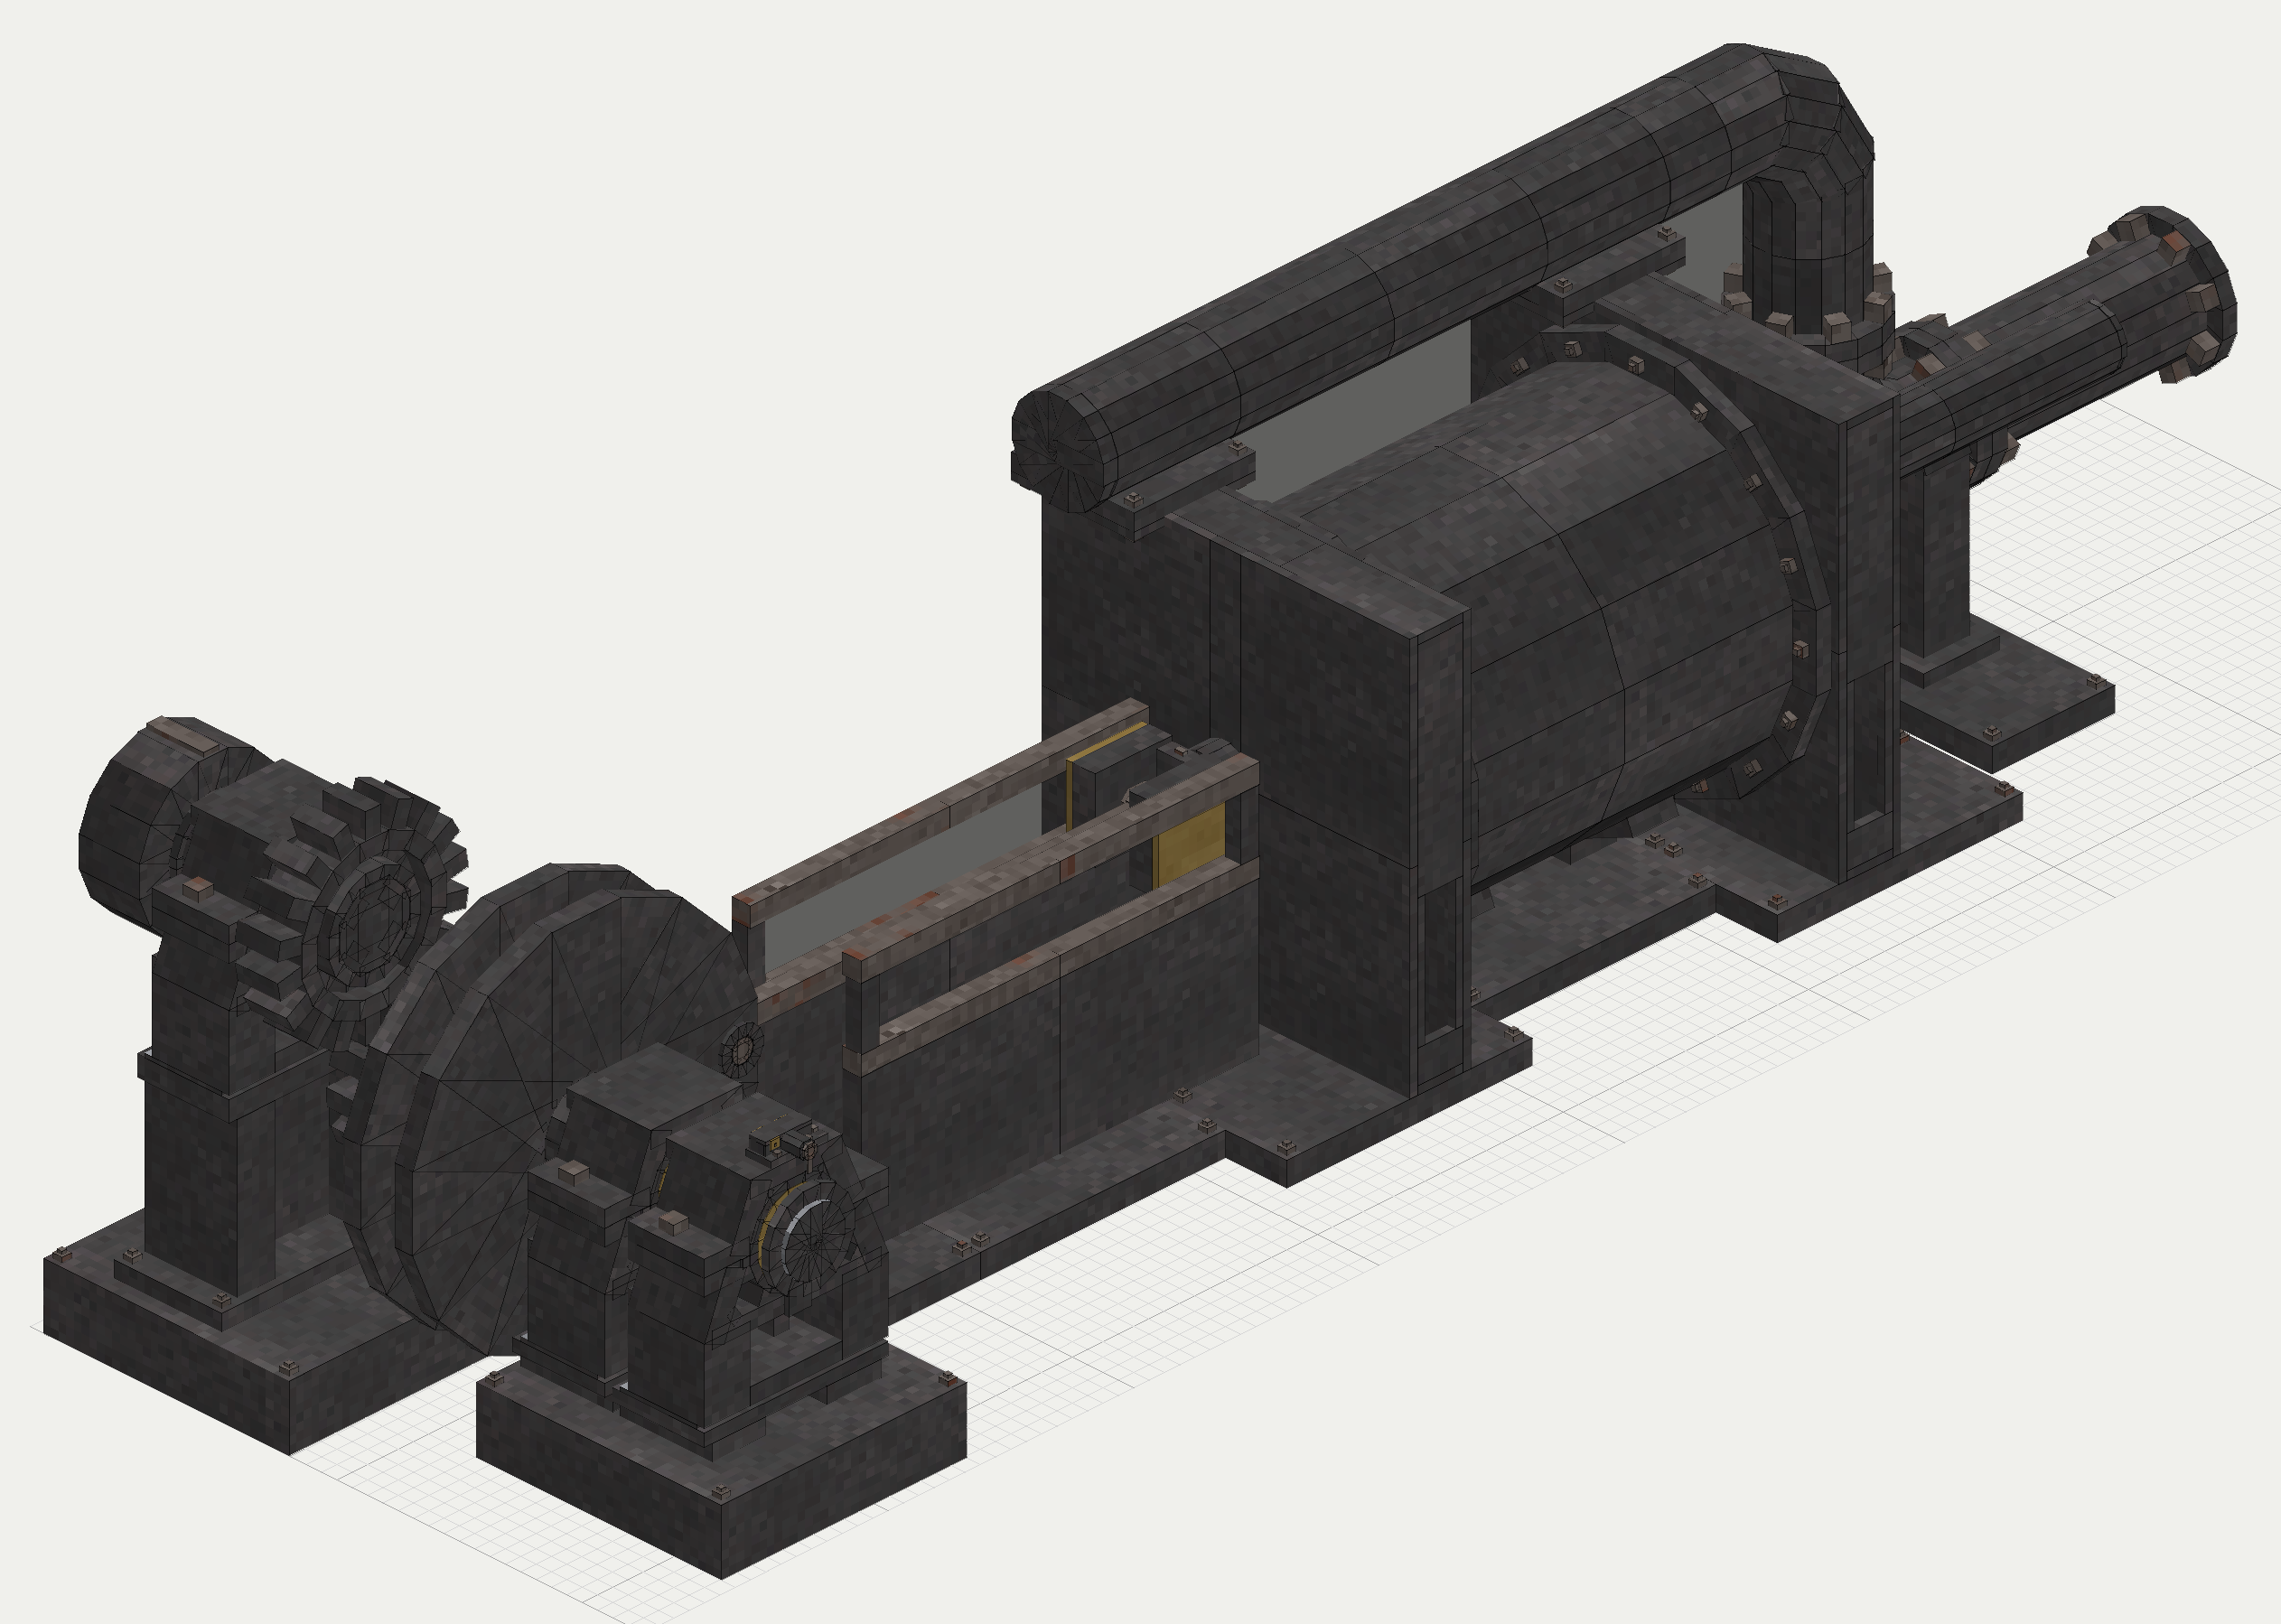

The machine takes cast parts: the cylinder, a piston, turned rods, brass bushes, bored standards and plates. How much air it delivers at which shaft speeds, and what pressure it holds against the cast main's rating, is not yet set.