
Shaft power and the flywheel
as of 0.8.0
The forming shop runs on a second power network, separate from vanilla mechanical power. Vanilla mechanical power has no storage: a waterwheel's output is a speed, available or not. A rolling pass wants far more torque for two seconds than any period prime mover makes continuously. This network stores that, in a flywheel. The machines it drives are in Rolling and the forming shop.
The five pieces
| Piece | What it does |
|---|---|
| flywheel | the reservoir; no vanilla axle couples to it |
| Cast Iron Shaft | the run itself; each segment carries rotating mass of its own |
| Cast Iron Bevel Gear | the corner |
| transmission | a 2 by 2 gearbox, and the only place two separate runs meet |
| Rolling Mill Axle | the bus cells a machine takes its drive on |
The flywheel
The flywheel is a vertical disc on a horizontal shaft, in two sizes and two orientations. The normal disc claims a clear 3 by 3 by 1 volume; the large one claims 5 by 5 by 2. Placement is refused unless the whole volume is clear.
The flywheel is storage only. No vanilla axle couples to it, and a waterwheel or windmill on a vanilla axle cannot feed the run; the prime mover is the iron breast wheel on a rapid stream, and later an engine joins the line.
| Quantity | Normal disc | Large disc |
|---|---|---|
| volume claimed | 3 x 3 x 1 | 5 x 5 x 2 |
| inertia | 10 | 150 |
| energy held at full speed | 20 | 300 |
Energy held is one half of the inertia times the square of the network's maximum speed, which is 2. The large wheel holds about fifteen times what the normal one does and takes about fifteen times as long to spin up, because inertia sets both.
A flywheel is inertia, not a battery. A drive that cannot out-torque the load plus the standing friction never spins it up at all, so a pulse cannot be trickle-charged. Standing resistance at full speed is 0.6 N.m, and whatever drive the run has beyond that is its headroom. A hot rolling pass draws 0.34 N.m of it.
There are no verbs on a flywheel. Looking at it prints the charge, the speed, the supply and the draw. The disc holds still for now; the planned redrawn wheel turns at the run's speed, so its visible rate is the reservoir's charge.
Shaft, bevel and transmission
A Cast Iron Shaft segment adds 2.8 of rotating mass to its run, so a shaft line rides jitter a little on its own without a dedicated flywheel. Segments run north-south, east-west or vertically.
A bevel is made in place: hold a Cast Iron Bevel Gear against a shaft and it consumes one gear and swaps that cell for a bevel on the same axis. A bevel connects on every face, and its branches follow whatever perpendicular shafts are placed against it, with no face to pick and no support to choose.
The transmission is three shipped variants: x2 and x4, which are always coupled and have no
verbs at all, and clutch, whose lever cell is right-clicked to engage or disengage. A disengaged
clutch leaves the two runs fully independent and shows it, one main shaft turning while the other
stands still. Each transmission is made as a frame at the Vice Bench and raised in place with its shafts, gears or cones and, on the belt transmission, a belt.
Gears mesh at a 2% loss.
Step by step
- Clear a 3 by 3 by 1 volume and place a flywheel in it.
- Build an Iron Breast Wheel where a rapid stream can be led to its pentrough, open its sluice a quarter at a time with a right-click (a sneak right-click closes one), and set the disengaging coupling at its port.
- Run Cast Iron Shaft from the flywheel toward the machines, turning corners with bevels.
- Seat each machine so its own two drive faces lie on the shaft line.
- Let the wheel spin up before working anything. Look at it: the charge readout is the gauge.
What goes wrong
A machine refuses to work rather than working slowly. A machine on a stopped run refuses outright, by design. Spin the run up first.
The run will not spin up at all. The drive cannot out-torque the load plus 0.6 N.m of standing friction. Shed machines from the line, or add drive, before adding a bigger flywheel: a bigger wheel makes the problem worse, not better, because it takes longer to reach speed.
The flywheel refuses to place. Something is in the disc's volume. All 9 cells of a normal wheel, or 50 of a large one, must be clear.
A bevel will not connect. It connects on every face; the shaft it should connect to is not perpendicular to it, or is not adjacent.
Planned
This section is planned and not yet in the game; until it lands, the rules above apply.
Two shaft sizes
Shafting will come in two sizes, each with its own supports, couplings, bevels and pulleys. The main shaft is cast iron, 250 mm across, and runs from the engine to the heavy machines. The line shaft is wrought iron, 125 mm across, and runs through the shop. The shaft in the game today becomes the main size. Both cross a block face at its centre.
| line shaft | main shaft | |
|---|---|---|
| made from | a rolled round, journals turned at the lathe or by hand at the Vice Bench | a cast shaft blank, journals turned at the lathe or by hand at the Vice Bench |
| rating | 3.4 kN*m | 17.0 kN*m |
| power at rating, 2 rad/s | 6.8 kW | 34 kW |
| span between supports | 3 blocks | 4 blocks |
| overhang past the last support | 1 block | 2 blocks |
| weight of one block | 94.5 kg | 353 kg |
A main meets a line only through a reducing coupling, a cast box bored 4 voxels at one end and 2 at the other and finished at the bench. A main set against a line without one is refused. A bevel junction whose through shaft is one size and whose branch the other joins them as well, and so does a frame or a belt. The Watt engine's 2.4 kNm passes a line shaft; the horizontal engine's 3.5 kNm strains it, and a cold rolling pass with its standing torque, 4 kN*m, wants a main.
Shafts as physical parts
Each shaft block will have its own mass, inertia and standing friction, taken from its size, so a long light line costs real torque merely to turn: 4.3 Nm a block on a line, 32.5 on a main. A run of 40 main blocks stands at 1.3 kNm, more than a single vanilla waterwheel gives. Shafting alone stores almost nothing; the flywheel still holds the energy.
A shaft needs support. A pedestal on the floor, a hanger to a beam above or a wall box to a side stands under it, and so do a machine port, a flywheel, a transmission frame, the disengaging coupling and a bevel junction's arm. No two supports lie farther apart than the span in the table and no free end overhangs past its allowance. A placement that breaks the rule is refused with the span named, and removing a support drops the blocks it leaves unsupported. Supports are part of a shaft's cost.
A segment over its rating takes permanent set; it creaks as the strain builds, shows the percent on the HUD, and parts if the load is held, at once at the shaft's ultimate strength. A parted shaft stays as a sheared block and splits the run. A server option turns parting off.
Couplings
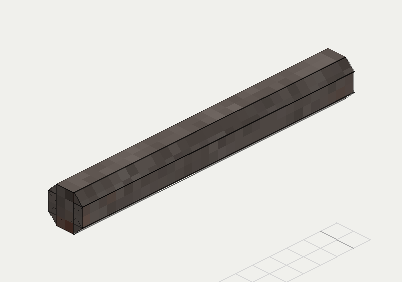
A joint between two shaft lengths is a half-lap coupling drawn beside each support, one to a span, with no item of its own, and none drawn where a junction or another support shares the face: each shaft length's recipe carries a coupling's iron. On the line size the box is 4.8 voxels across and 4 long, twice the shaft's diameter, and the shaft swells under it.
The disengaging coupling joins the breast wheel's main to the line, and an engine beside it; its claws overrun when the engine runs ahead. It gains a lever. A weighted lever and fork throws it out and back in on a right-click. Thrown out, the wheel turns free and the shafting stops; engaged, it drives and still overruns when the shafting runs ahead. The weight holds the lever over centre either way. The claws drive one way, so the block comes in a mirrored variant for the other hand, chosen when it is placed.
Bevel and mitre junctions
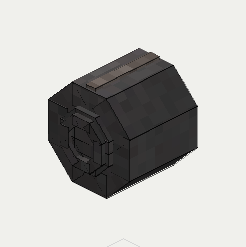
A bevel junction will gear one cross axis only: the through shaft and up to two branches on opposite faces, 1:1. A neighbouring shaft on the other cross axis is not geared. This replaces the rule above that a bevel connects on every face. Fitting the crown wheel is done once with the bevel gear, and each geared branch takes a pinion of its own.
Every junction carries one wheel pattern, 24 teeth, bored to its shaft: the crown to the through shaft's size and each pinion to its branch's. A wheel bored for the line fits only a line junction. A line junction stands in the same hangers, pedestals and wall boxes as a main one. The teeth are rated by breadth and radius, 4.1 kN*m on a main junction; a geared line shaft is held to the lower of that and the line's own 3.4. The Watt engine's torque passes both; the horizontal engine's passes a main junction and strains a line one. A branch over its rating strips its own pinion.
On cast-iron machines every pair of crossed shafts is a cast bevel wheel, or a cast mitre wheel at 1:1, moulded with its teeth: the horizontal engine's governor train is one. The wooden machines keep their star plates.
Gears and pulleys bored to order
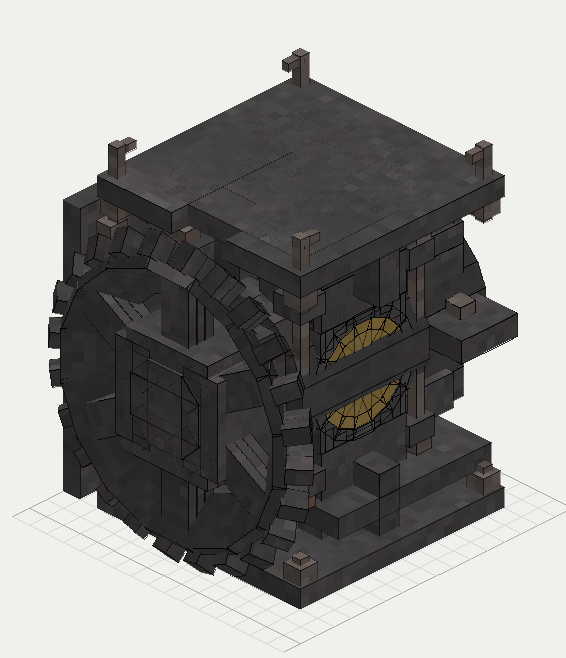
A bevel gear is cast from one blank and its eye is bored at the lathe for the main or the line shaft; the finished gear carries that bore. A pulley is cast the same way, its hub bored at the drilling machine or the Vice Bench, and carries its bore beside its size.
A belt 4 voxels wide grips 0.39 kNm on a size 1 pulley and 1.3 kNm on a size 2. Past that it slips, carrying 0.8 of its cap, and the energy slipped wears the belt. A belt drives benches and machine tools, not a rolling pass or an engine.
The flywheel's burst limit
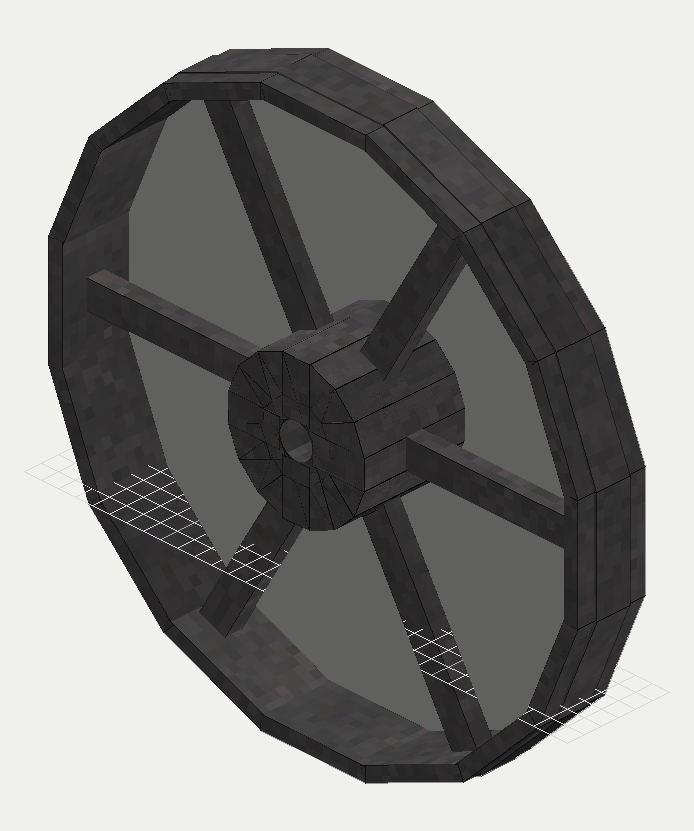
The flywheel becomes storage only, with a main-size shaft port at each axle end in place of its hub, the axle turning in two bored bearing housings. The wheel stands about a third sunk in a pit: the normal wheel drops one cell and the large wheel two, and placement is refused unless the pit's cells are clear as well as the wheel's. The pit has no lining of its own; its walls and floor are the blocks the player builds round it. Each wheel has a rim limit of 25 m/s: 18.5 rad/s for the normal wheel and 10.9 for the large. A run's guard is the lowest limit among its flywheels. Past it the rim speed shows in red and the wheel creaks; held there, it bursts, dropping as scrap, and the run loses its inertia. The server option that turns shaft parting off turns bursting off with it.
Machine ports
Every machine keeps its drive on a main-size port, and the vanilla ports on the machine tools go. The lathe, drilling machine, shaper, planer and boring machine run on a main at those ports, and the first need no pulley. The shear and the nail, rivet and heading machines take main-size ports as well, and so does the bender, which sits with the steam hammer for the plate it bends. Once a line runs, any of them and any machine tool takes a size 2 belt from it onto a pulley on its port shaft, none of their jobs asking over 0.5 kN*m. The rolling mill stays geared to a main: its pass is over every belt's grip. The lathe turns the line's own journals and the roll sets, so it needs no belt.
A machine farther from the player than a set distance, 48 blocks unless the player changes it, stops moving its parts and takes them up again in step with its drive when the player comes back within it. A setting of 0 never pauses.
Looking at a machine will name the part in each cell and, at a port, what it takes and whether it is connected. While a pipe, a shaft or a wrench is held, every port face in view carries a marker in its network's colour.
Pumps and the tub blower on shafting
Both pump tiers and the Tub Blast Machine take their drive and pipes at drawn ports. The wood pump and the wooden tub blower stay on vanilla mechanical power, driven by a vanilla axle, and meet pipes at plated mains. The cast pump takes a main-size shaft on one side and cast mains for its suction and delivery; its pinion drives a spur 2:1 down to a three-throw crank, a plunger to each throw. The delivery barrel carries the air vessel on a flanged neck cast on its top.