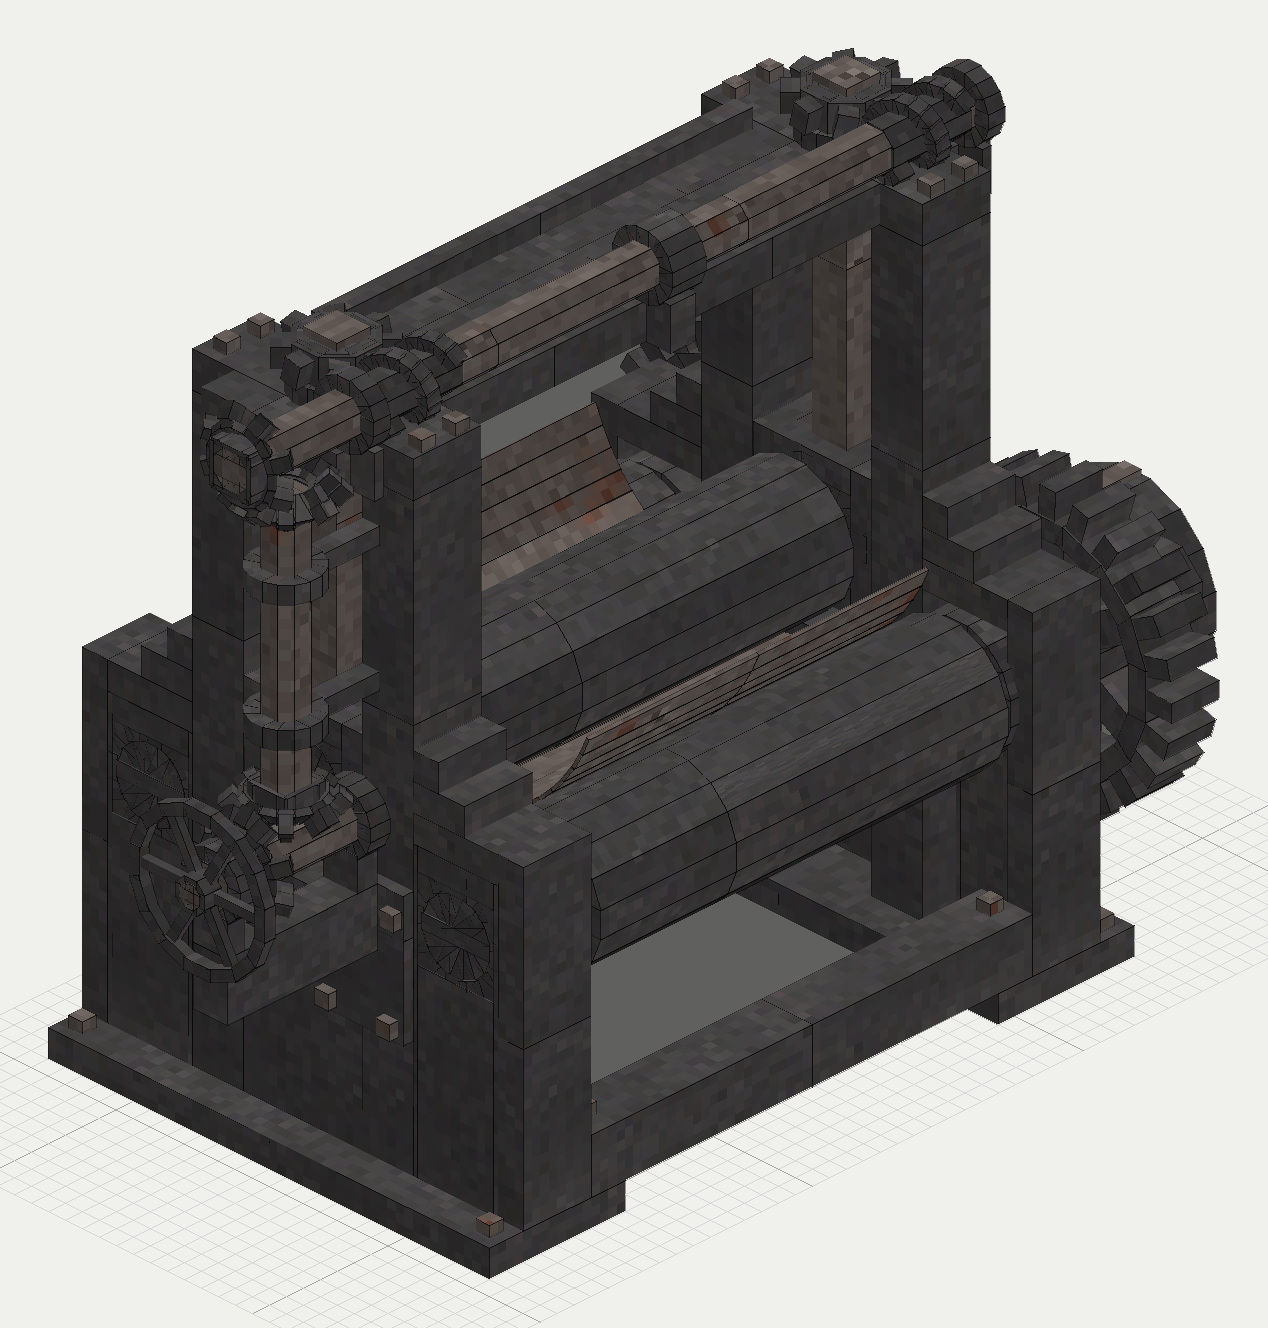
Rolling and the forming shop
as of 0.8.0
This shop is where iron stops being a lump and starts being parts. A furnace hands over a Shingled Bar, a Shingled Slab or a cast piece, and the machines work that raw shape down until a recipe can name it. None of them is swung by hand: every one takes its drive from a line of Cast Iron Shaft. See Shaft power and the flywheel.
A working shop is four things standing together: a drive strong enough for everything hung on it, a Rolling Mill to reduce, a Shearing Machine to crop, and a Heating furnace beside them so nothing has to be carried away to stay workable.
Heat is the governing rule
Iron rolls hot at 900 C and above. Below that two things happen at once, and both of them stop a pass.
- The bite collapses. How deep a pass can cut is the square of the friction times the roll radius, and cold iron grips about thirty times worse, so a cold piece will not enter the rolls at all.
- The flow stress climbs. A fully cold piece resists ten times as hard as a hot one, rising over the 400 C below rolling heat, so a cooling piece both refuses to bite and loads the drive harder.
Stock cools while it is worked, and it cools whether or not it is moving, so a jam is self-worsening. Cooling and reheating run on the same law: the rate goes with surface area over volume, so a thin piece cools faster than a thick one and also reheats faster. A shingled bar fresh off the helve is still above rolling heat after about 25 seconds on the mill floor.
The Rolling Mill
The mill is the only reducing machine, and it never makes a finished piece: it makes thinner stock, and everything goes on to the shear from there.
- Fit a roll set by right-clicking the machine with the set in hand. It hands back whatever was fitted before, and refuses mid-pass.
- Lay stock on the input deck. On the flat and grooved sets, where along the deck the click lands picks the gap: the deck is split into equal bands, one per gap the set carries. The wide set has no bands: hold right click on the cell above either end of the stand to lower its top roller, or hold right click while sneaking to raise it, between a 1.0 and a 2.5 gap, and the stock goes through at the gap you set.
- Right-click the near side of the piece, or sneak plus right-click the far side, to choose which side goes through.
- The stand draws 0.34 N.m off the run while stock is between the rolls, and nothing when it is empty.
A gap is walked in two rounds, one feed per side, and the gauge moves only on the feed that completes the round, so the piece is one thickness across its width at every moment it can be seen. Nothing is committed mid-pass: losing the drive, letting the stock go cold, breaking the mill or freeing the piece with a wrench all leave the reduction unapplied and the gap simply redone.
The schedule has to be walked rung by rung. The deepest legal bite is 0.36, a round's draft is 0.25 and a gap is a 0.5 step, so the next rung is the only rung that will bite. Nothing checks the ordering; friction does the checking.
Five refusals, each naming a different fix:
| Refusal | Means |
|---|---|
| no roll set | nothing is fitted |
| wrong form | this set does not roll this shape |
| no reduction | the gap is wider than the stock, so it would pass through untouched |
| will not bite | the gap is deeper than the bite limit; step back a rung |
| too cold | the piece is below 900 C; take it back to the heat |
A stall is not a lost pass. The mill resumes where it stopped once the run spins back up or the stock is reheated. A stalled piece keeps cooling, though, so past the bite threshold the only answer is the furnace.
The Shearing Machine
Every crop in the shop passes through this one block, which is why the mill has no claim gesture at all. Seat a blade set in the nest, right-click stock against the throat, and one stroke takes one finished piece off and hands the rest back as stock at the same gauge. Sneak plus right-click takes the blade set back.
| Input | With a set of this family | Yields |
|---|---|---|
| Shingled Bar at stage 2.0 | grooved | 4 vanilla iron rods |
| Beam Blank at stage 1.0 | flatwide | 2 vanilla iron plates |
| Shingled Slab at stage 2.0 | flatwide | 2 Heavy Plate |
| Rolled Rod at stage 1.0 | grooved | 4 Rivet Rod |
| a vanilla iron plate | any | 2 Nail Plate |
A piece that has been started on cannot go back through the mill. Finish the cuts, then roll the pieces on.
Shearing is temperature-free: a cold cut is allowed and asks twice the job's own drive requirement, because shearing needs force rather than friction and cold metal parts more cleanly than hot. Cold cutting is a power achievement, not a tier gate, which is what keeps the reheat furnace an economy rather than a wall.
The fastener benches
The nail machine and the rivet heading machine are the same machine wearing different tooling. Fit a Die and right-click the bench with the blank it wants; a die names the machine it belongs to, so a nail die in a rivet heading machine has no work and says so.
| Bench | Blank | Yields | Drive | Seconds |
|---|---|---|---|---|
| nail machine | Nail Plate | 4 bundles of vanilla nails and strips | 0.2 N.m | 2 |
| rivet heading machine | Rivet Rod | 2 bundles of Rivets | 0.3 N.m | 3 |
Both are whole-item jobs: the blank is consumed and every bundle leaves at once, with no remainder. Rivets go twice as far as nails out of the same iron, which is why the nail machine is deliberately the cheaper machine to build. Wherever a joint only has to hold, either will do; wherever it also has to be tight, a boiler shell above all, only rivets are accepted.
Keeping stock hot
A vanilla forge tops out at an ingot and cannot hold a slab at all. The Heating furnace is the shop's answer: build it up from its core, lay pieces along its Heating Hearth rows, and light the Firebox. Anything lying on the hearth climbs back toward rolling heat while the player works.
Right-click a hearth cell with a stock piece to lay it in that row, right-click empty-handed to take it back. The hearth is three rows and a loaded centre row blocks both flanks, going in and coming out, so the flanks are loaded first and drawn last and a full hearth unloads centre-first.
Reheating is at roughly a vanilla forge's rate per piece, with no multiplier of its own: a shingled bar takes about 40 seconds and a shingled slab about 58. The rate is set by the piece's section, surface over volume, so a thin piece both heats and cools faster than a thick one. What the hearth is for is that it holds three pieces at once and takes shapes a forge refuses.
Long stock keeps in a Storage Rack, which fills by the length of what is leaned in it rather than by the piece.
What goes wrong
Nothing can be rolled. No roll set is craftable in survival. The three sets that ship, flat, wide flat and grooved, exist as items and are read by the mill's fit gesture, but survival grants none of them.
Stock that went cold cannot be reheated. Only Shingled Bar, Shingled Slab and the three cast stock pieces have hearth art and are admitted. Rolled Rod, Beam Blank and Heavy Plate Blank are refused by the hearth, and a vanilla forge takes none of them either. A piece on one of those routes can still be sheared, because shearing is temperature-free, but it can never be rolled on.
The mill refuses a piece that looks right. Read the refusal. "No reduction" and "will not bite" are opposite problems: one gap is too wide and the other too deep.
The deck click lands on the wrong gap. On the flat and grooved sets the bands run along the barrel. Click nearer the far end for the wider gaps. The wide set ignores where the click lands and rolls at the gap its top roller is screwed to.
A machine on the line does nothing. The run is stopped, or it cannot carry what is hung on it. Lay in the drive before filling the line with machines.
Planned
This section is planned and not yet in the game; until it lands, the rules above apply.
Drive: main ports and line belts
Every machine of the shop will take its drive from a main-size port, so the shop runs on cast main before any line shaft exists: the shear, the bender, the nail machine, the rivet machine and every machine tool all work that way. Once a line runs, any of them can instead take a size 2 belt from it onto a pulley on its port shaft. A size 2 belt grips 1.3 kN.m and slips past that, and none of these jobs asks more than 0.5 kN.m, so the belt is never the limit for them.
The Rolling Mill is the exception. Its pass asks more than any belt holds, so it stays geared to a main, and its cold pass, with standing torque of 4.0 kN.m, still fits under what a cast main carries. That is why the mill can be the first machine of the shop, before a line exists to hang a belt from.
The bending machine takes a main-size port as well, but it sits with the steam hammer rather than the mill: the boilerplate and heavy plate it bends come from the hammer's slab.
The mill as a merchant stand
The mill is drawn as a merchant stand of the period, not as a rolling plant. Its rolls are half a block across on a barrel one block long, about the size merchant rolls had: a few feet long and under half a metre across, against plate rolls twice that length. It rolls bar, rod and plate up to 15 voxels across, and no wider. Its rolls and pinions are drawn as sixteen-sided rounds, as every round part six or more voxels across will be. Where a cast-iron machine has two shafts crossing, the crossing takes a cast mitre or bevel wheel.
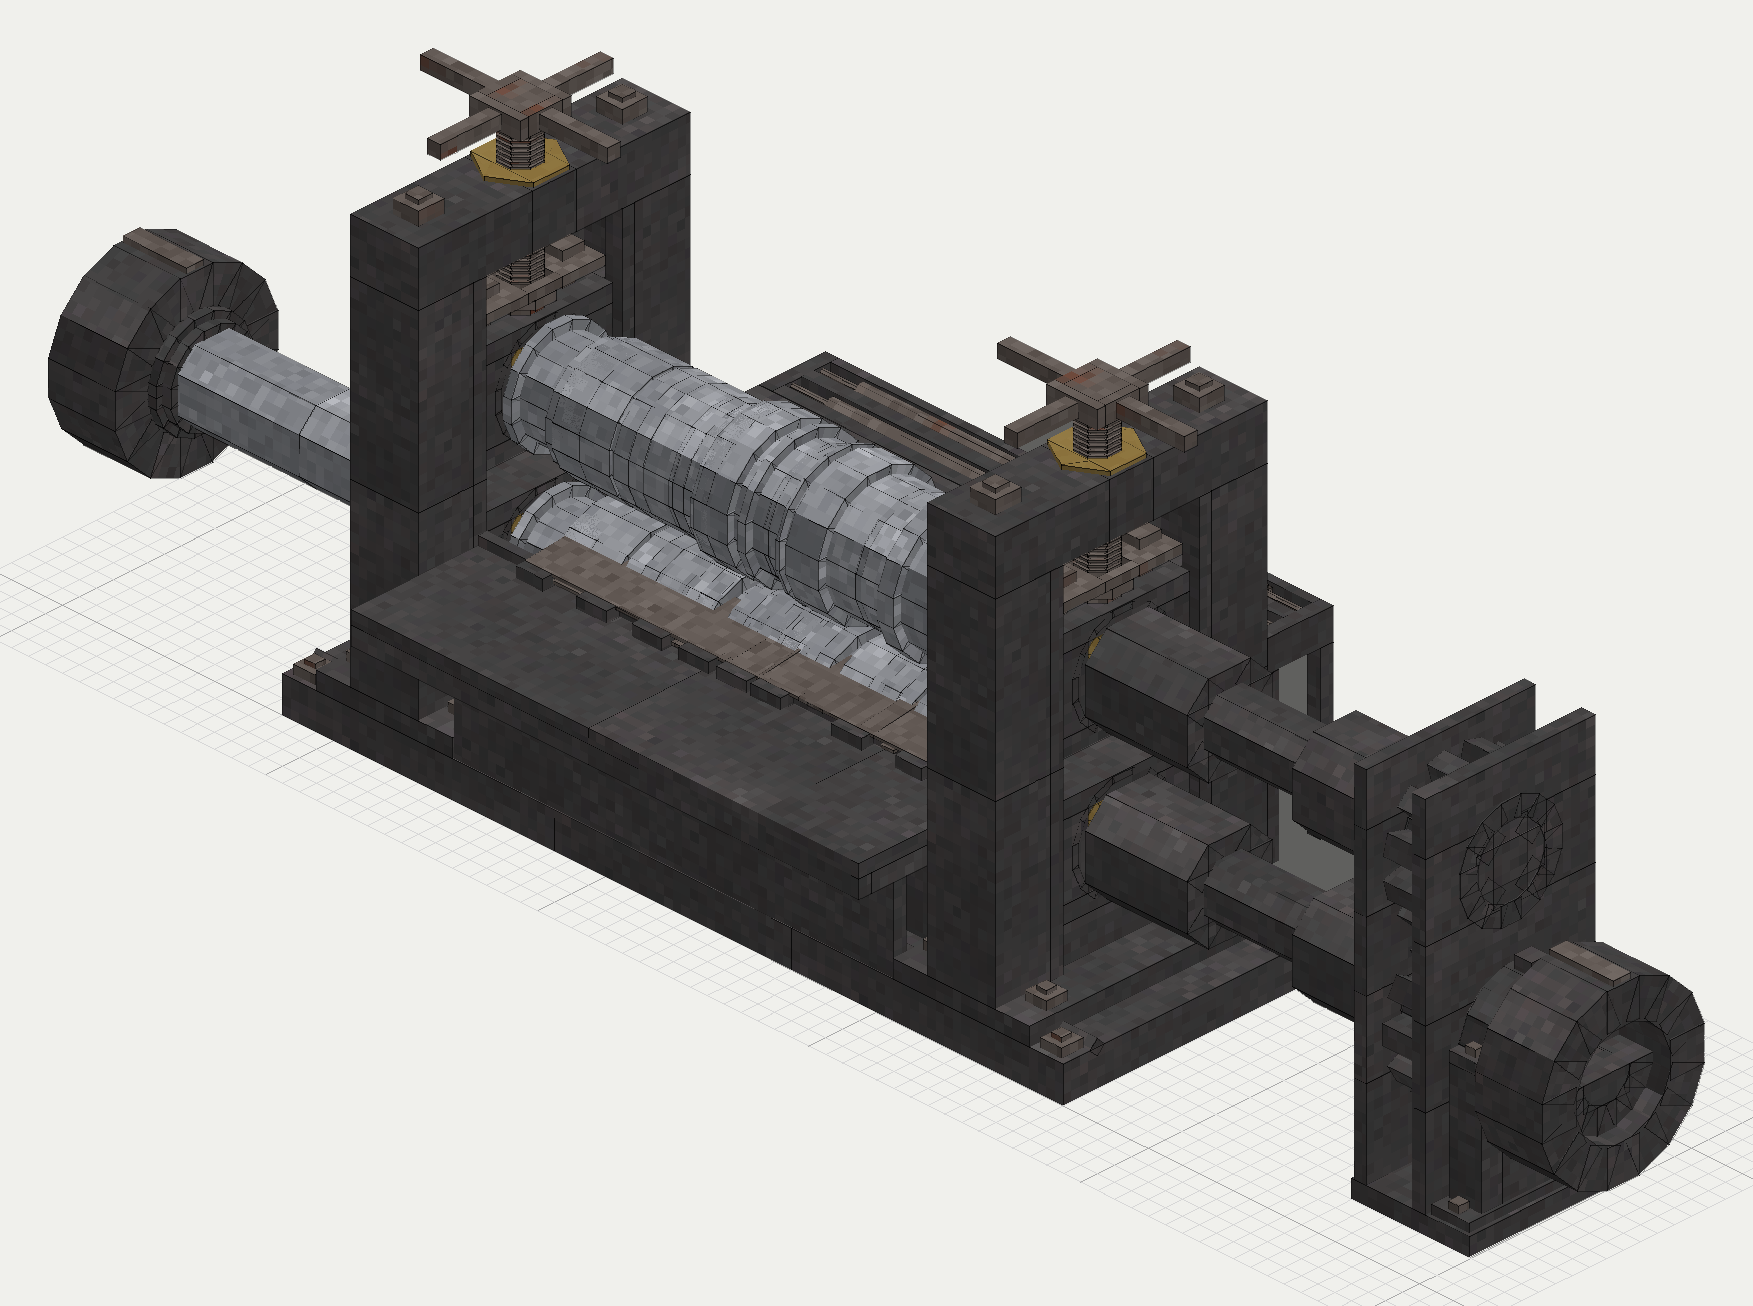
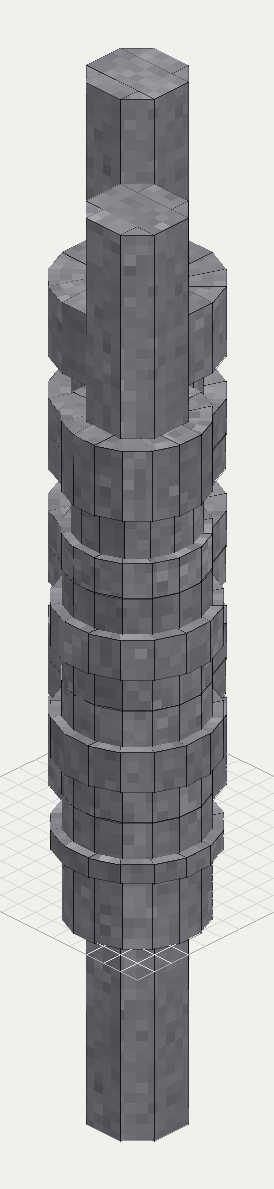
The Wide Flat Roll Set is a plain barrel over the whole sixteen voxels, the gap set by the screws, as period sheet and boiler-plate rolls were. The Flat Roll Set is collared: four flat grooves cut in the barrel, a pair for the bar and a pair for the rod, each about as wide as the piece at that step, with thin collars between them. Plate from a beam is rolled on the wide set, not the flat one.


The boring machine
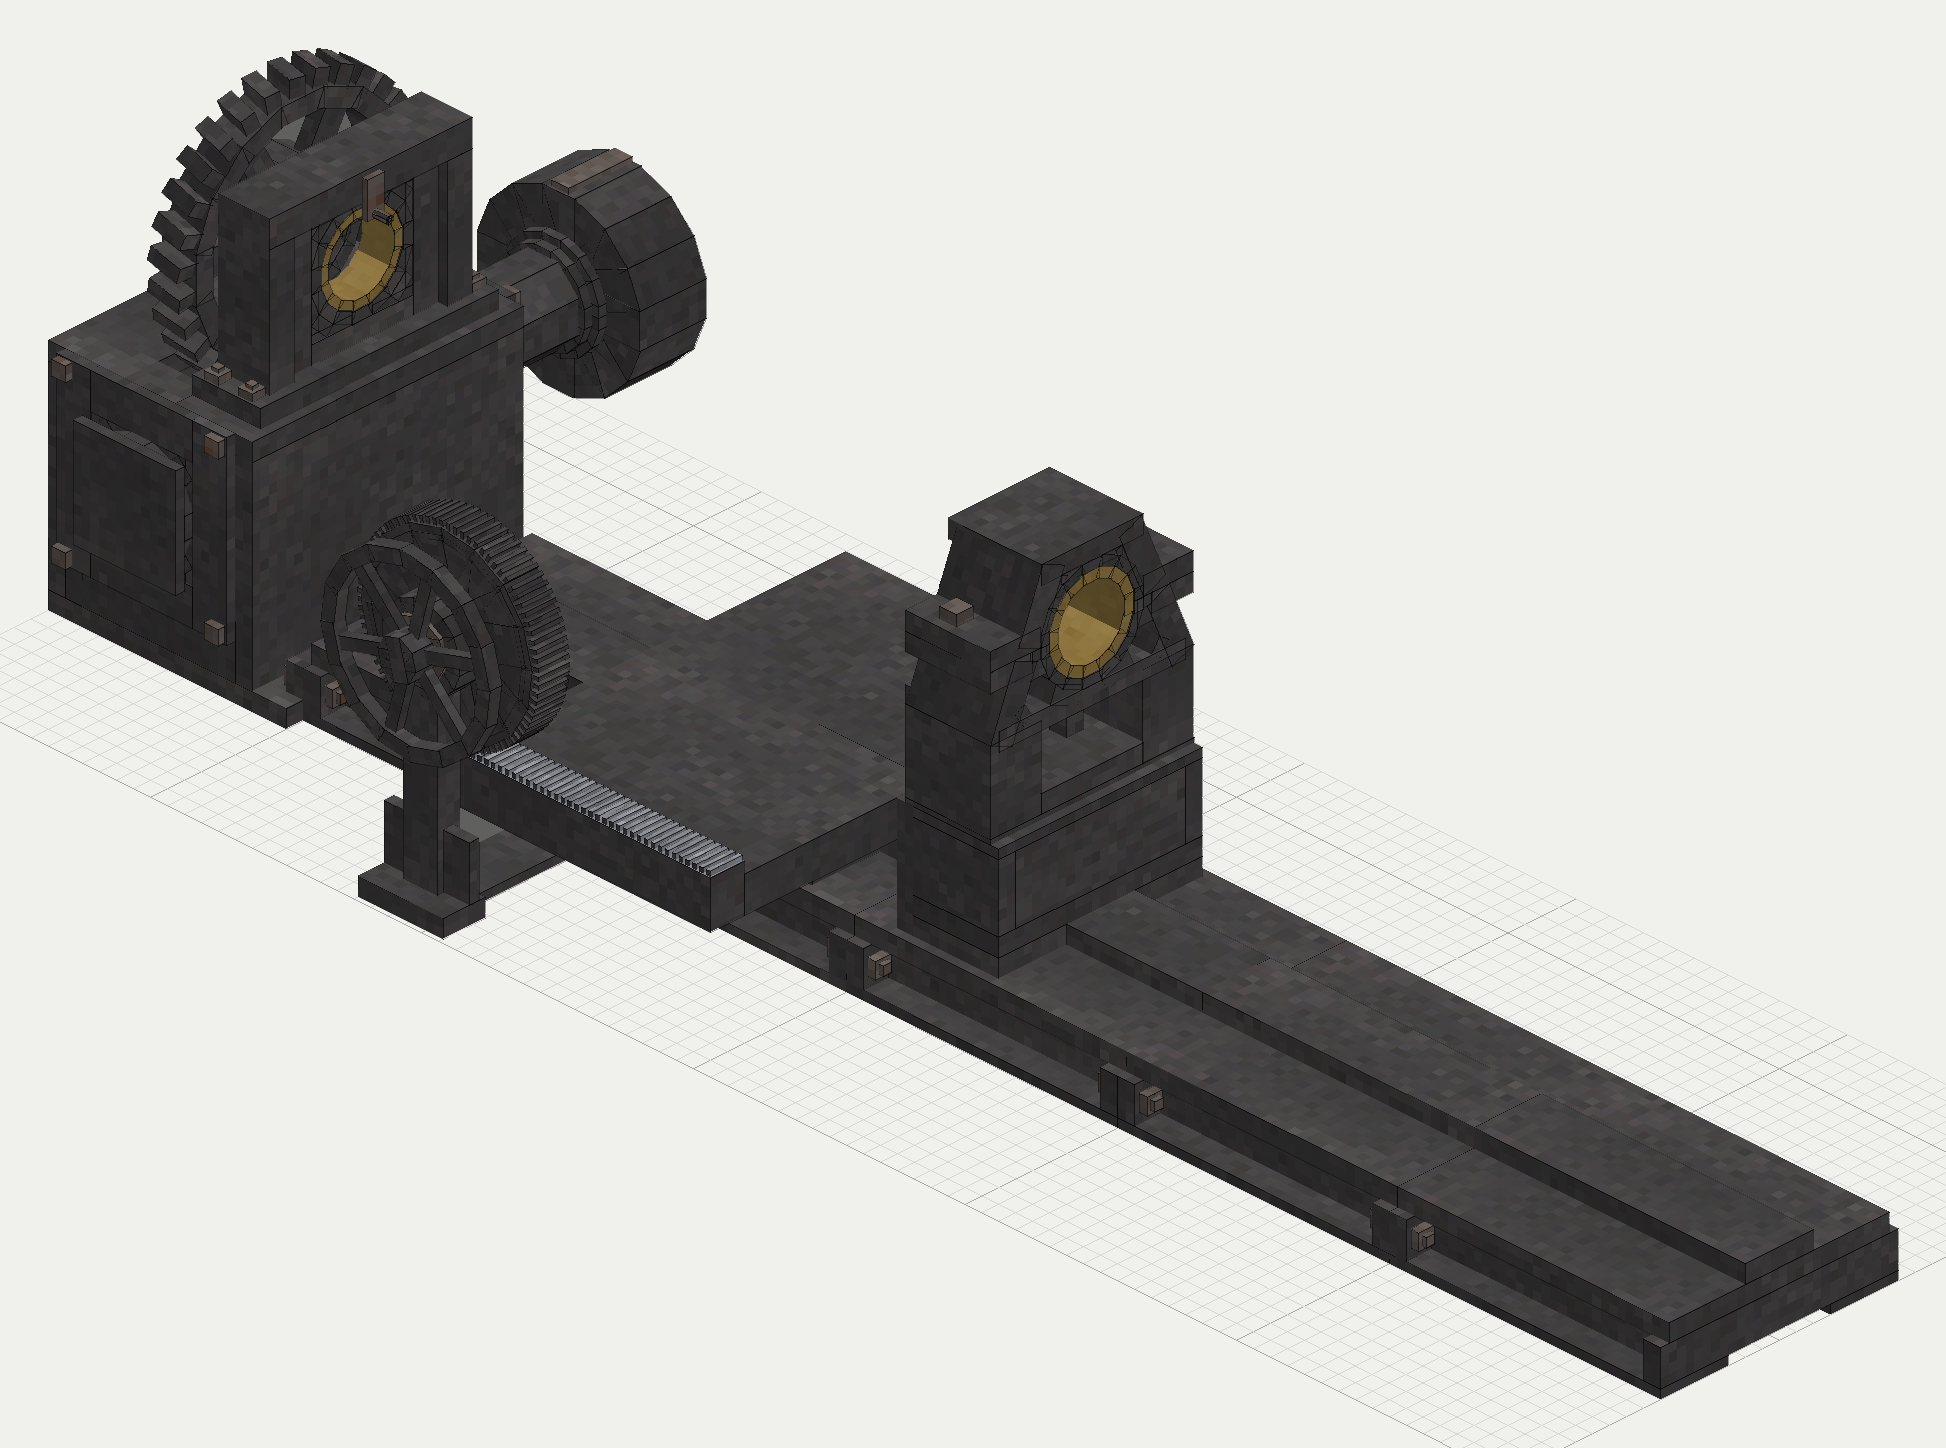
The bed and its rail will run one block further east, so that the standard at the bed's east end can slide back off the end of the bar. Loading follows the way a period shop did it: when the window takes a cylinder or gives one back, the outboard standard slides east along the rail past the bar's end, the work is carried on or off the bar to the table, and the standard slides back. The footprint is one cell longer for it. A cylinder is bored here and nowhere else; no bench job bores one, so the first engine, the feed pump and the steam hammer wait for this machine.

The planer
The planer will also face the mating surfaces of cast parts that bolt to one another: the feet of the cast standards, the joint faces of valve bodies and the plates of engine beds. Their bills ask for these faces planed, so a casting fresh from the flask is not ready to bolt down until it has been through the planer. Planing the slide bar from a vanilla iron rod is its other job in the same bills.
The steam hammer's sole
The sole plate of the Steam Hammer will be one casting, as the sole of a period hammer was, about 3 m by 2.2 m. It is paid in Heavy Cast Plate, as many plates as its drawn volume measures at the plate's density: the sole is drawn 4.5 blocks by 3 blocks and a quarter of a block thick, open a little over a block square round the anvil. The frame standards, hammer mass and anvil block stay cast iron as before; the piston, rod and lever stay steel or wrought iron, and the dies stay forged, never cast. The hammer also shingles the slab that the Wide Flat Roll Set rolls into boilerplate and heavy plate, so the bending machine and the boilerplate build of the Cornish boiler open with it.
The bending machine
The bending machine bends boilerplate and heavy plate into boiler shells and wheel rims on a pyramid of three rolls. The roll set is the wide flat one, and the height the top roller is screwed to selects the bend. Its bent shells and rims are later routes to parts the small flask already pours.