Bending Machine
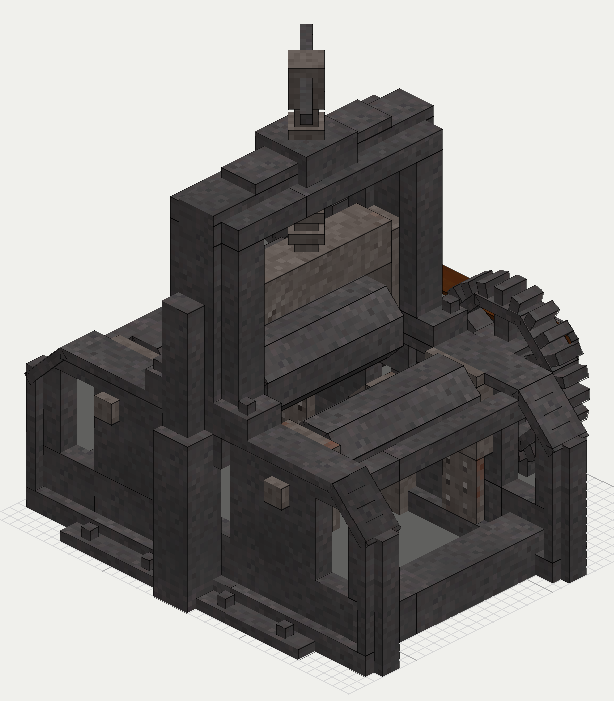
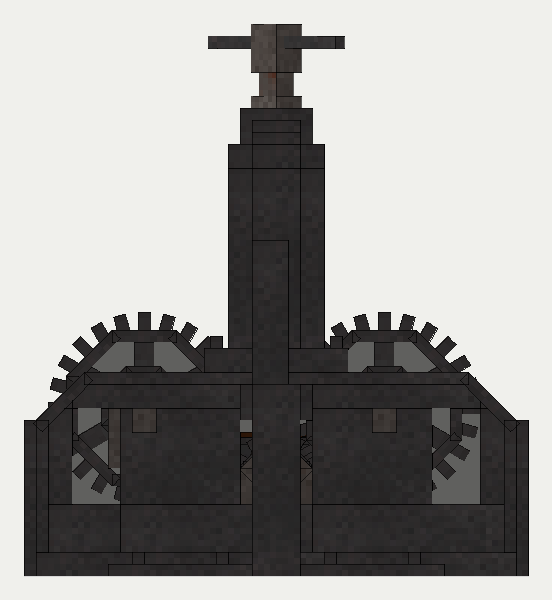
Three power rolls that curve plate, boilerplate, rod and beam over several passes. The fitted tool - conical, cylindrical or large-radius - picks the curve, and the drive direction picks the feed side. The bending process is not built yet.
Three power rolls in a triangle curve plate, boilerplate, rod and beam over several passes rather than reducing them the way the Rolling Mill does. The tool fitted, not the machine, picks the curve: conical for pipe skelp, cylindrical for shells and barrels, large-radius for wheel rims. Feed a piece in and hold the roller-gap cell to close the gap for another pass; which side is the input follows the drive direction.
See Rolling and the forming shop for where it sits among the line's other machines.
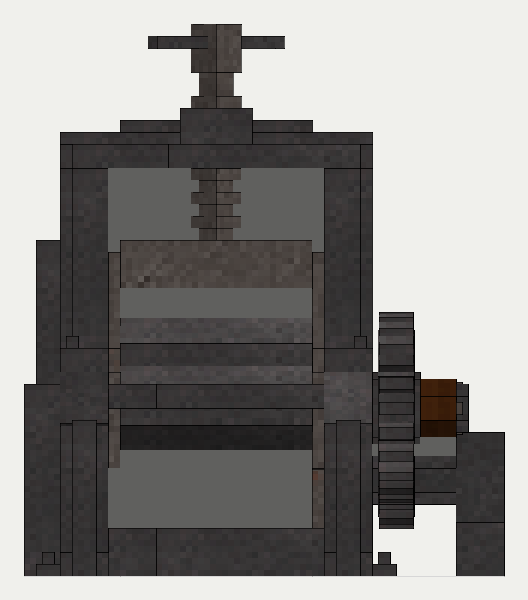
 front
 right
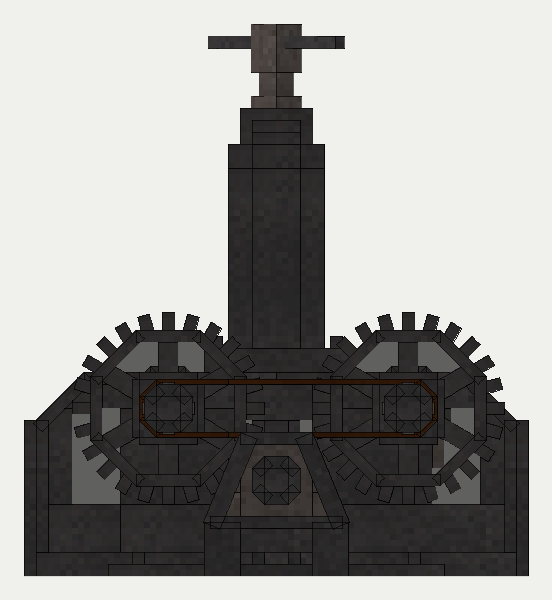 back
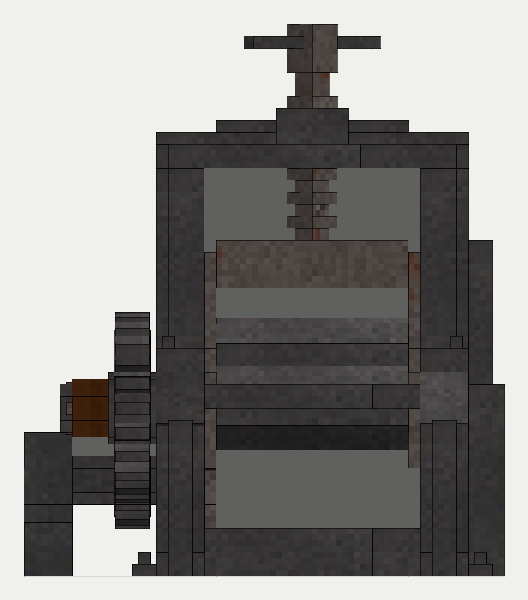 left
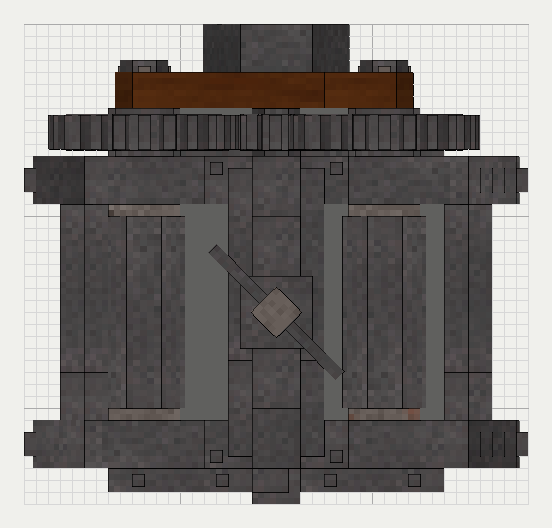 top