
Long Flask
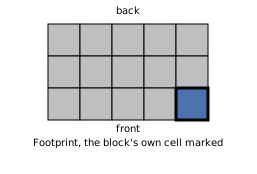
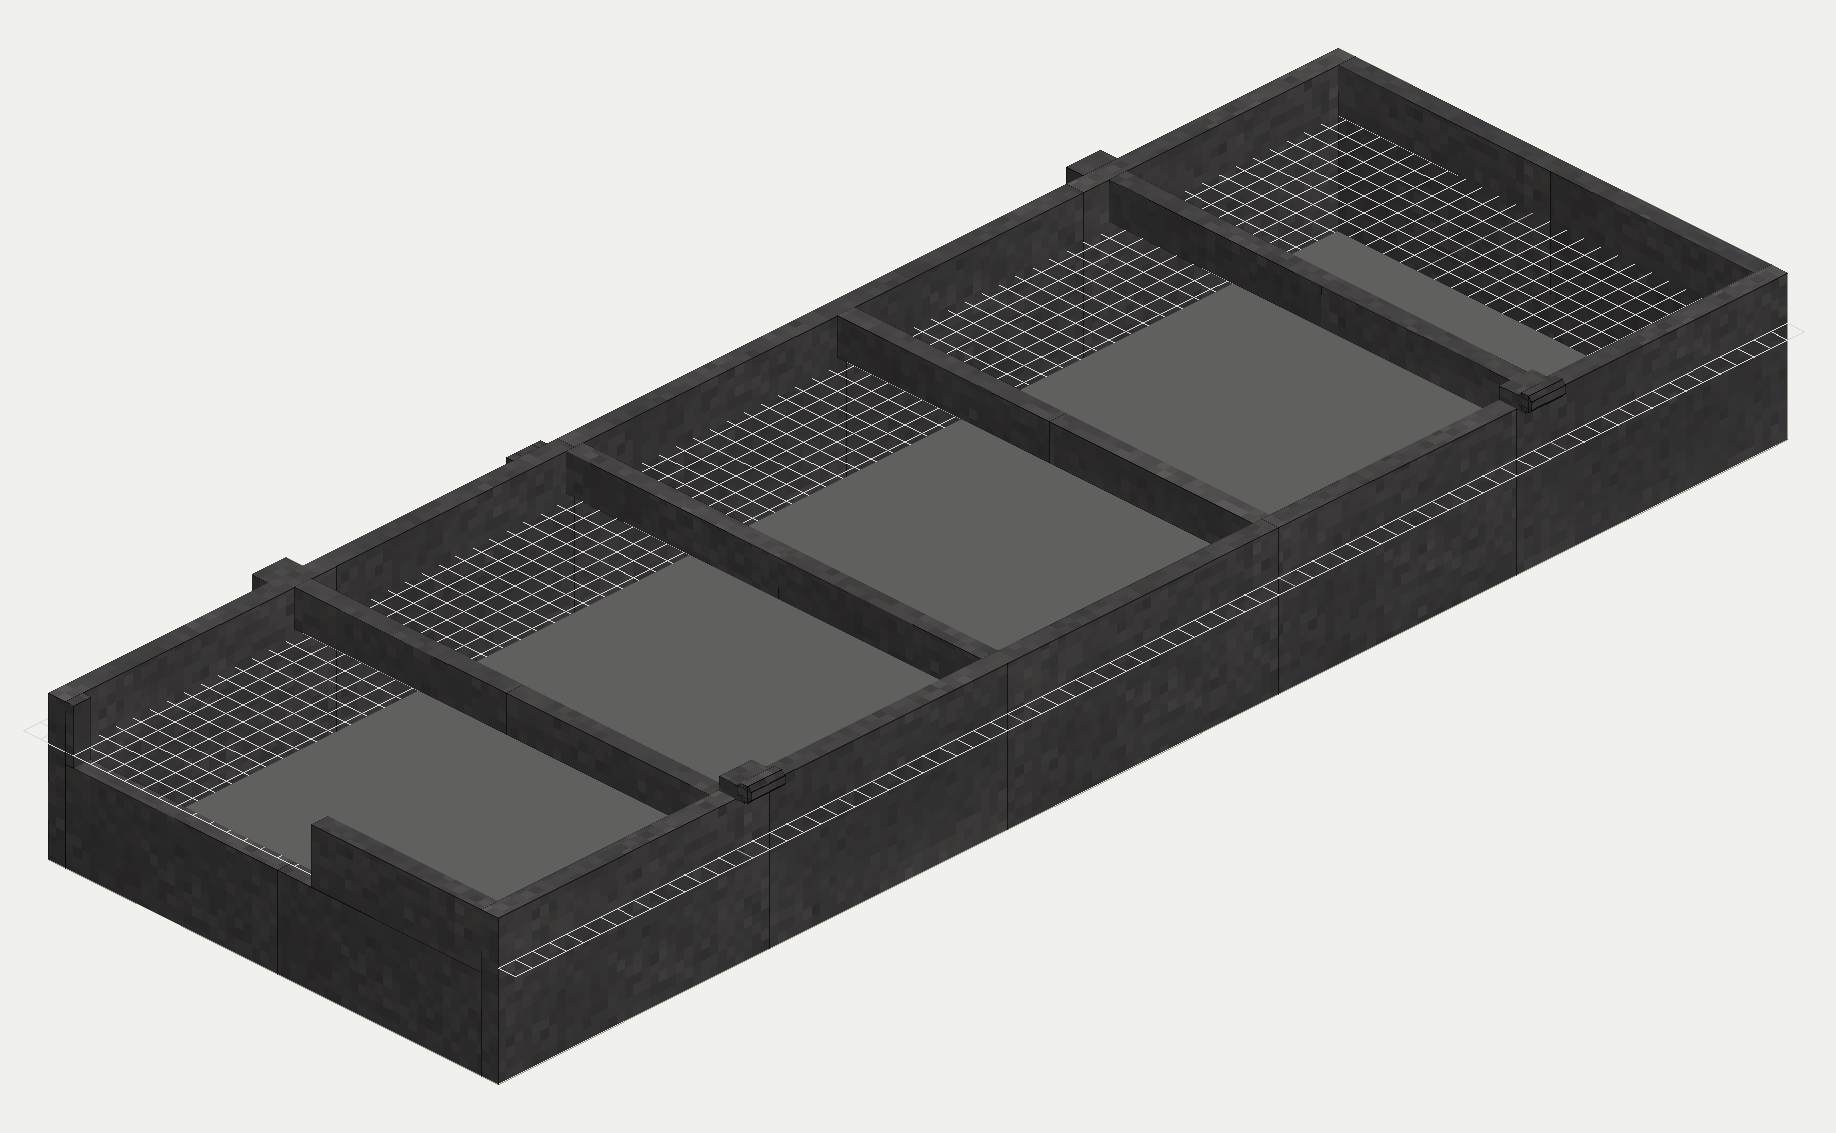
The long flask is the sand-casting station for long and big parts: it spans two blocks across and four long, and reads its pattern the same way the plain Small Flask does, sand rammed in once, a pattern pressed after. It refuses a pattern with no long flask entry just as firmly as the small flask refuses one cut for it, so which station a part wants is fixed by its pattern rather than by choice.
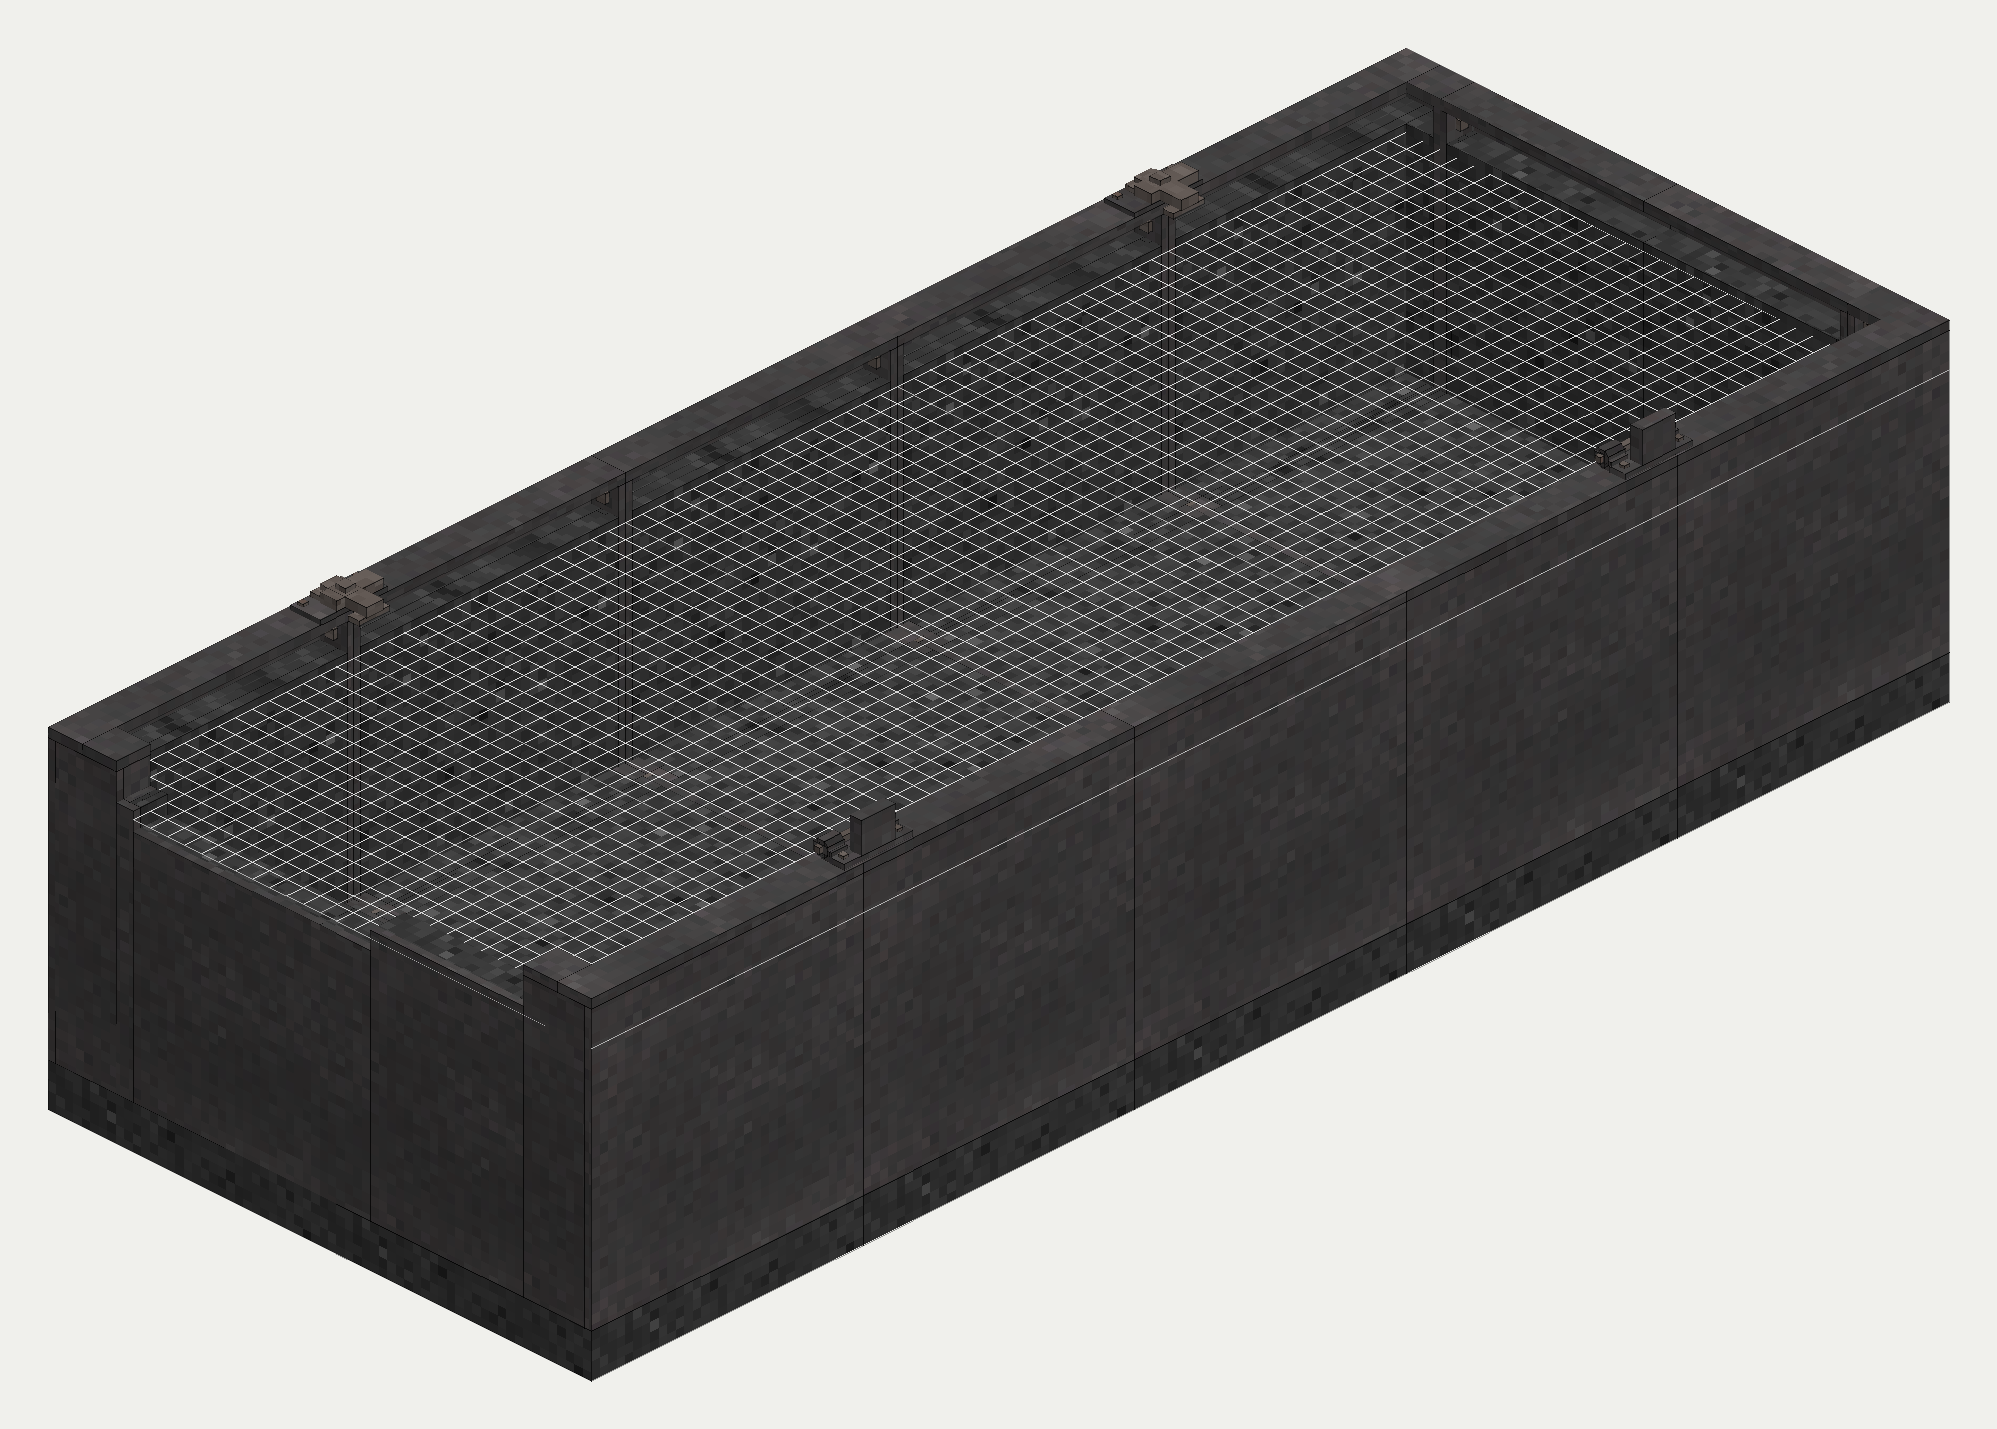
See Molten metal and casting for the ram, impression, fill and shake cycle every flask shares.
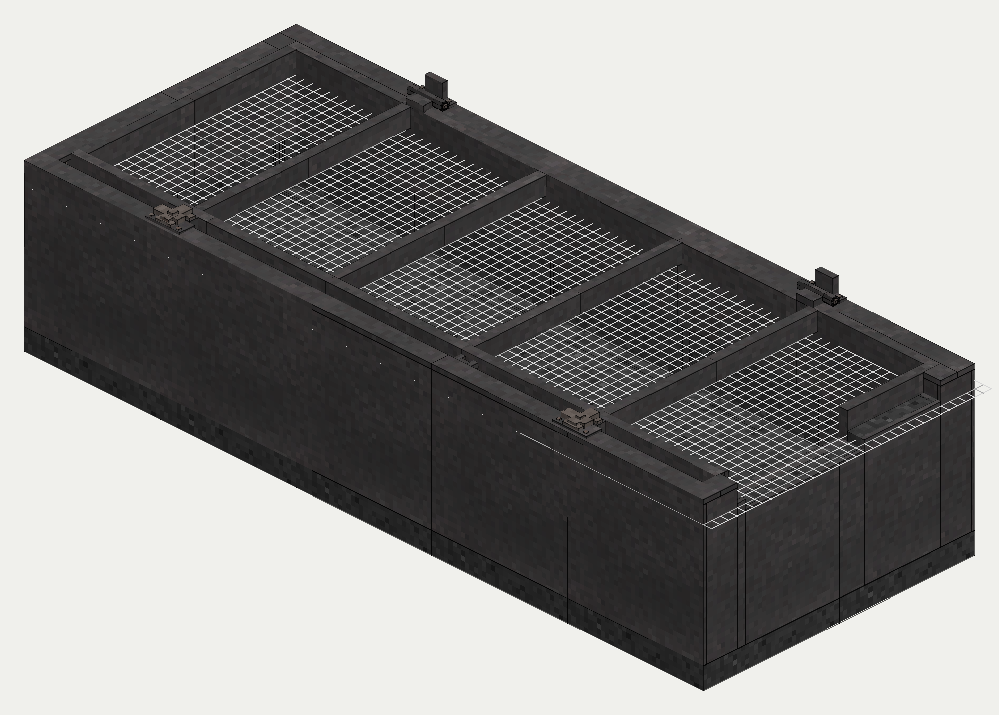
 front
 right
 back
 left
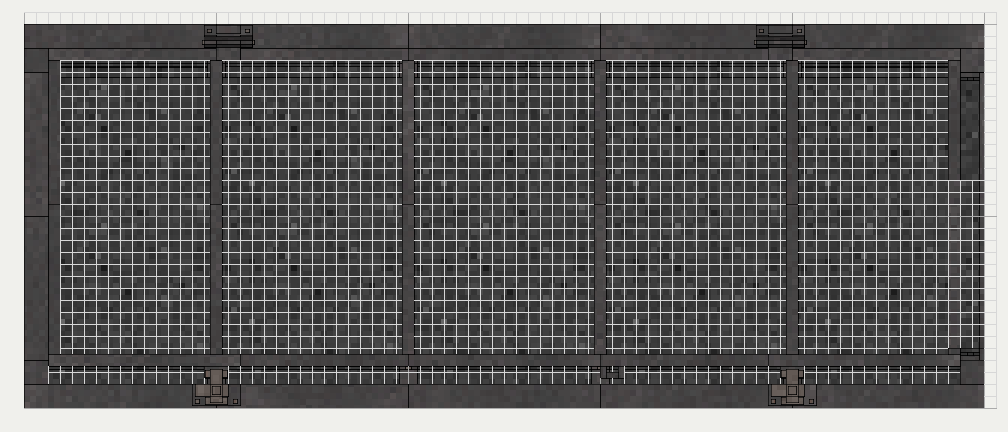 top
Made by
| any Brick x 6 | any Brick x 6 | any Brick x 6 | any Brick x 6 | any Brick x 6 |
| any Brick x 6 | Fire clay x 4 | Fire clay x 4 | any Brick x 6 | |
| Mortar x 6 | any Brick x 6 | Fire clay x 4 | any Brick x 6 | Mortar x 6 |
| any Brick x 6 | Fire clay x 4 | any Brick x 6 | ||
| any Brick x 6 | any Brick x 6 | any Brick x 6 | any Brick x 6 | any Brick x 6 |
| Long Flask | ||||
Needs: 16 Fire clay, 96 any Brick, 12 Mortar; makes 1 Long Flask
| Fireclay brick x 6 | Fireclay brick x 6 | Fireclay brick x 6 | Fireclay brick x 6 | Fireclay brick x 6 |
| Fireclay brick x 6 | Fire clay x 4 | Fire clay x 4 | Fireclay brick x 6 | |
| Mortar x 6 | Fireclay brick x 6 | Fire clay x 4 | Fireclay brick x 6 | Mortar x 6 |
| Fireclay brick x 6 | Fire clay x 4 | Fireclay brick x 6 | ||
| Fireclay brick x 6 | Fireclay brick x 6 | Fireclay brick x 6 | Fireclay brick x 6 | Fireclay brick x 6 |
| Long Flask | ||||
Needs: 16 Fire clay, 96 Fireclay brick, 12 Mortar; makes 1 Long Flask
Amounts are the mod's defaults; the recipe-cost level changes them (see recipe cost levels).
Built in place
| Stage | Materials |
|---|---|
| 1 | none |
| 2 | Drag Cross Bar x 4 |
| 3 | Drag Side Section x 3, Drag Left Corner, Drag Right Corner, Bolts and Nuts x 2, Nails and strips (Iron) |
| 4 | Drag Side Section x 3, Drag Left Corner, Drag Right Corner, Bolts and Nuts x 2, Nails and strips (Iron) |
| 5 | Drag North End, Bolts and Nuts |
| 6 | Drag South End, Bolts and Nuts |
| 7 | Cope East Side Half Casting x 2, Cope West Side Half Casting, Cope Staple Side Half Casting, Cope Plain Side Casting x 2, Cope North End Casting, Cope South End Casting, Cope Cross Bar Casting x 4, Cope Hinge Leaf Casting x 2, Cope Anchor Plate Casting x 2 |
| 8 | Bolts and Nuts x 8, Iron rod x 4 |
Needs: 4 Drag Cross Bar, 6 Drag Side Section, 2 Drag Left Corner, 2 Drag Right Corner, 14 Bolts and Nuts, 2 Nails and strips (Iron), 1 Drag North End, 1 Drag South End, 2 Cope East Side Half Casting, 1 Cope West Side Half Casting, 1 Cope Staple Side Half Casting, 2 Cope Plain Side Casting, 1 Cope North End Casting, 1 Cope South End Casting, 4 Cope Cross Bar Casting, 2 Cope Hinge Leaf Casting, 2 Cope Anchor Plate Casting, 4 Iron rod
Amounts are the mod's defaults; the recipe-cost level changes them (see recipe cost levels).
Crafting chain
- Sand and blue clay go into the crafting grid, eight sand and one clay to eight Green Sand.
- The Flask Diagram, drafted at the Drawing Table, goes in the bench's diagram slot at the Vice Bench, with 96 bricks of one colour, or 96 fire bricks, 12 mortar and 16 fire clay laid in the crafting grid in the long flask's pattern; a hammer held on the bench works the step, which gives the Long Flask. Placed, it stands as its bed of sand alone: the cast-iron drag is built up on it in turn, the cross bars, the west side, the east side, then the north end and the south end, before the cope or the sand is touched. The parts are Floor Flask castings; the bars take 4, a side takes 3 side sections, a left and a right corner, 2 bolts and a wedge strip, and each end takes its casting and a bolt.
- A pattern with a long flask entry is drafted as a diagram at the Drawing Table and cut with a knife from pattern boards; it is pressed into the Green Sand rammed into the placed flask, once for each piece of the part: a pattern of several pieces is pressed again for each, up to the flask's count, and the pour fills the pieces pressed. A pour that ran short yields the pieces it filled and scraps the rest; one that came in below the pattern's minimum temperature scraps all of it.
The cope
A closed pattern, one moulded from both sides, casts at the long flask only under its cope: a cast-iron lid on hinges along the flask's east wall. It is optional, and open work never needs it. The belly helve's helve, standards and cam ring are cast under it.

- Hang the cope once. Hold its cast parts against the built flask, then the eight bolts and four iron rods; the cope hangs thrown back and claims 24 cells above and beside the flask, its own two columns and the column east of it, which must be clear.
- Ram green sand into the drag and press the closed pattern. The first press strikes the sand level with the parting; a closed piece bedded in the drag refuses more sand, and a cope that stands closed refuses any pattern.
- Close the cope with an empty hand on its face, ram green sand into it, then drive the wedge of each of its two cramps with a hammer. The block info reads "Wedge the cope." and then "Ready to pour."
- Pour as at any flask. The flask draws metal only while the cope is closed and rammed. Poured unwedged, the cope lifts, the iron runs out at the joint and the whole pour is scrap.
- Once the iron is hard, knock the wedges out, lift the cope and shake the castings out with an empty hand. Lifting a wedged or liquid cope is refused, and so is shaking out under a closed one.